
In the pharmaceutical industry, the treatment of organic waste gas has always been a headache. Traditionalwaste gas treatmentNot only can not effectively solve the problem of waste gas, but also may bring high cost and waste of resources. So, is there an efficient, environmentally friendly and economical solution? This has to mention the membrane condensation technology.
Many pharmaceutical companies in the treatment of organic waste gas, often usedactivated charcoaladsorption andRTODevice. Although activated carbon adsorption can adsorb organic matter in waste gas, frequent replacement of activated carbon is not only costly, but also the waste carbon replaced is hazardous waste, the treatment procedures are cumbersome, and only the organic matter is transferred, which does not really solve the problem. Although the RTO equipment has a good treatment effect, it has a high operating cost, especially when dealing with low-concentration exhaust gas, the gas consumption is large, and even the value of the recovered solvent is not worth the cost of burning gas. In addition, the organic solvent in the waste gas is directly burned or adsorbed, resulting in a great waste of resources, but also increased the cost of environmental protection enterprises.
Membrane condensation technology has brought new hope for the treatment of organic waste gas in the pharmaceutical industry. to LuoyangWohong PetrochemicalTaking the membrane condensation recovery unit of Equipment Co., Ltd. as an example, it adopts a three-stage condensation processgas separation membraneThe combined process has many unique advantages.
The operation of the equipment only consumes electricity, and the refrigeration compressor and vacuum pump are controlled by frequency conversion, which can automatically adjust the power according to the exhaust gas load, effectively control the power consumption, and greatly reduce the operating cost.
The equipment can condense and liquefy the organic solvent in the waste gas for recovery, and the recovery purity can reach a higher level. The recovered solvent can be directly reused for production or external sales, and the environmental protection expenditure can be converted into economic benefits, which truly achieves two goals with one stone.
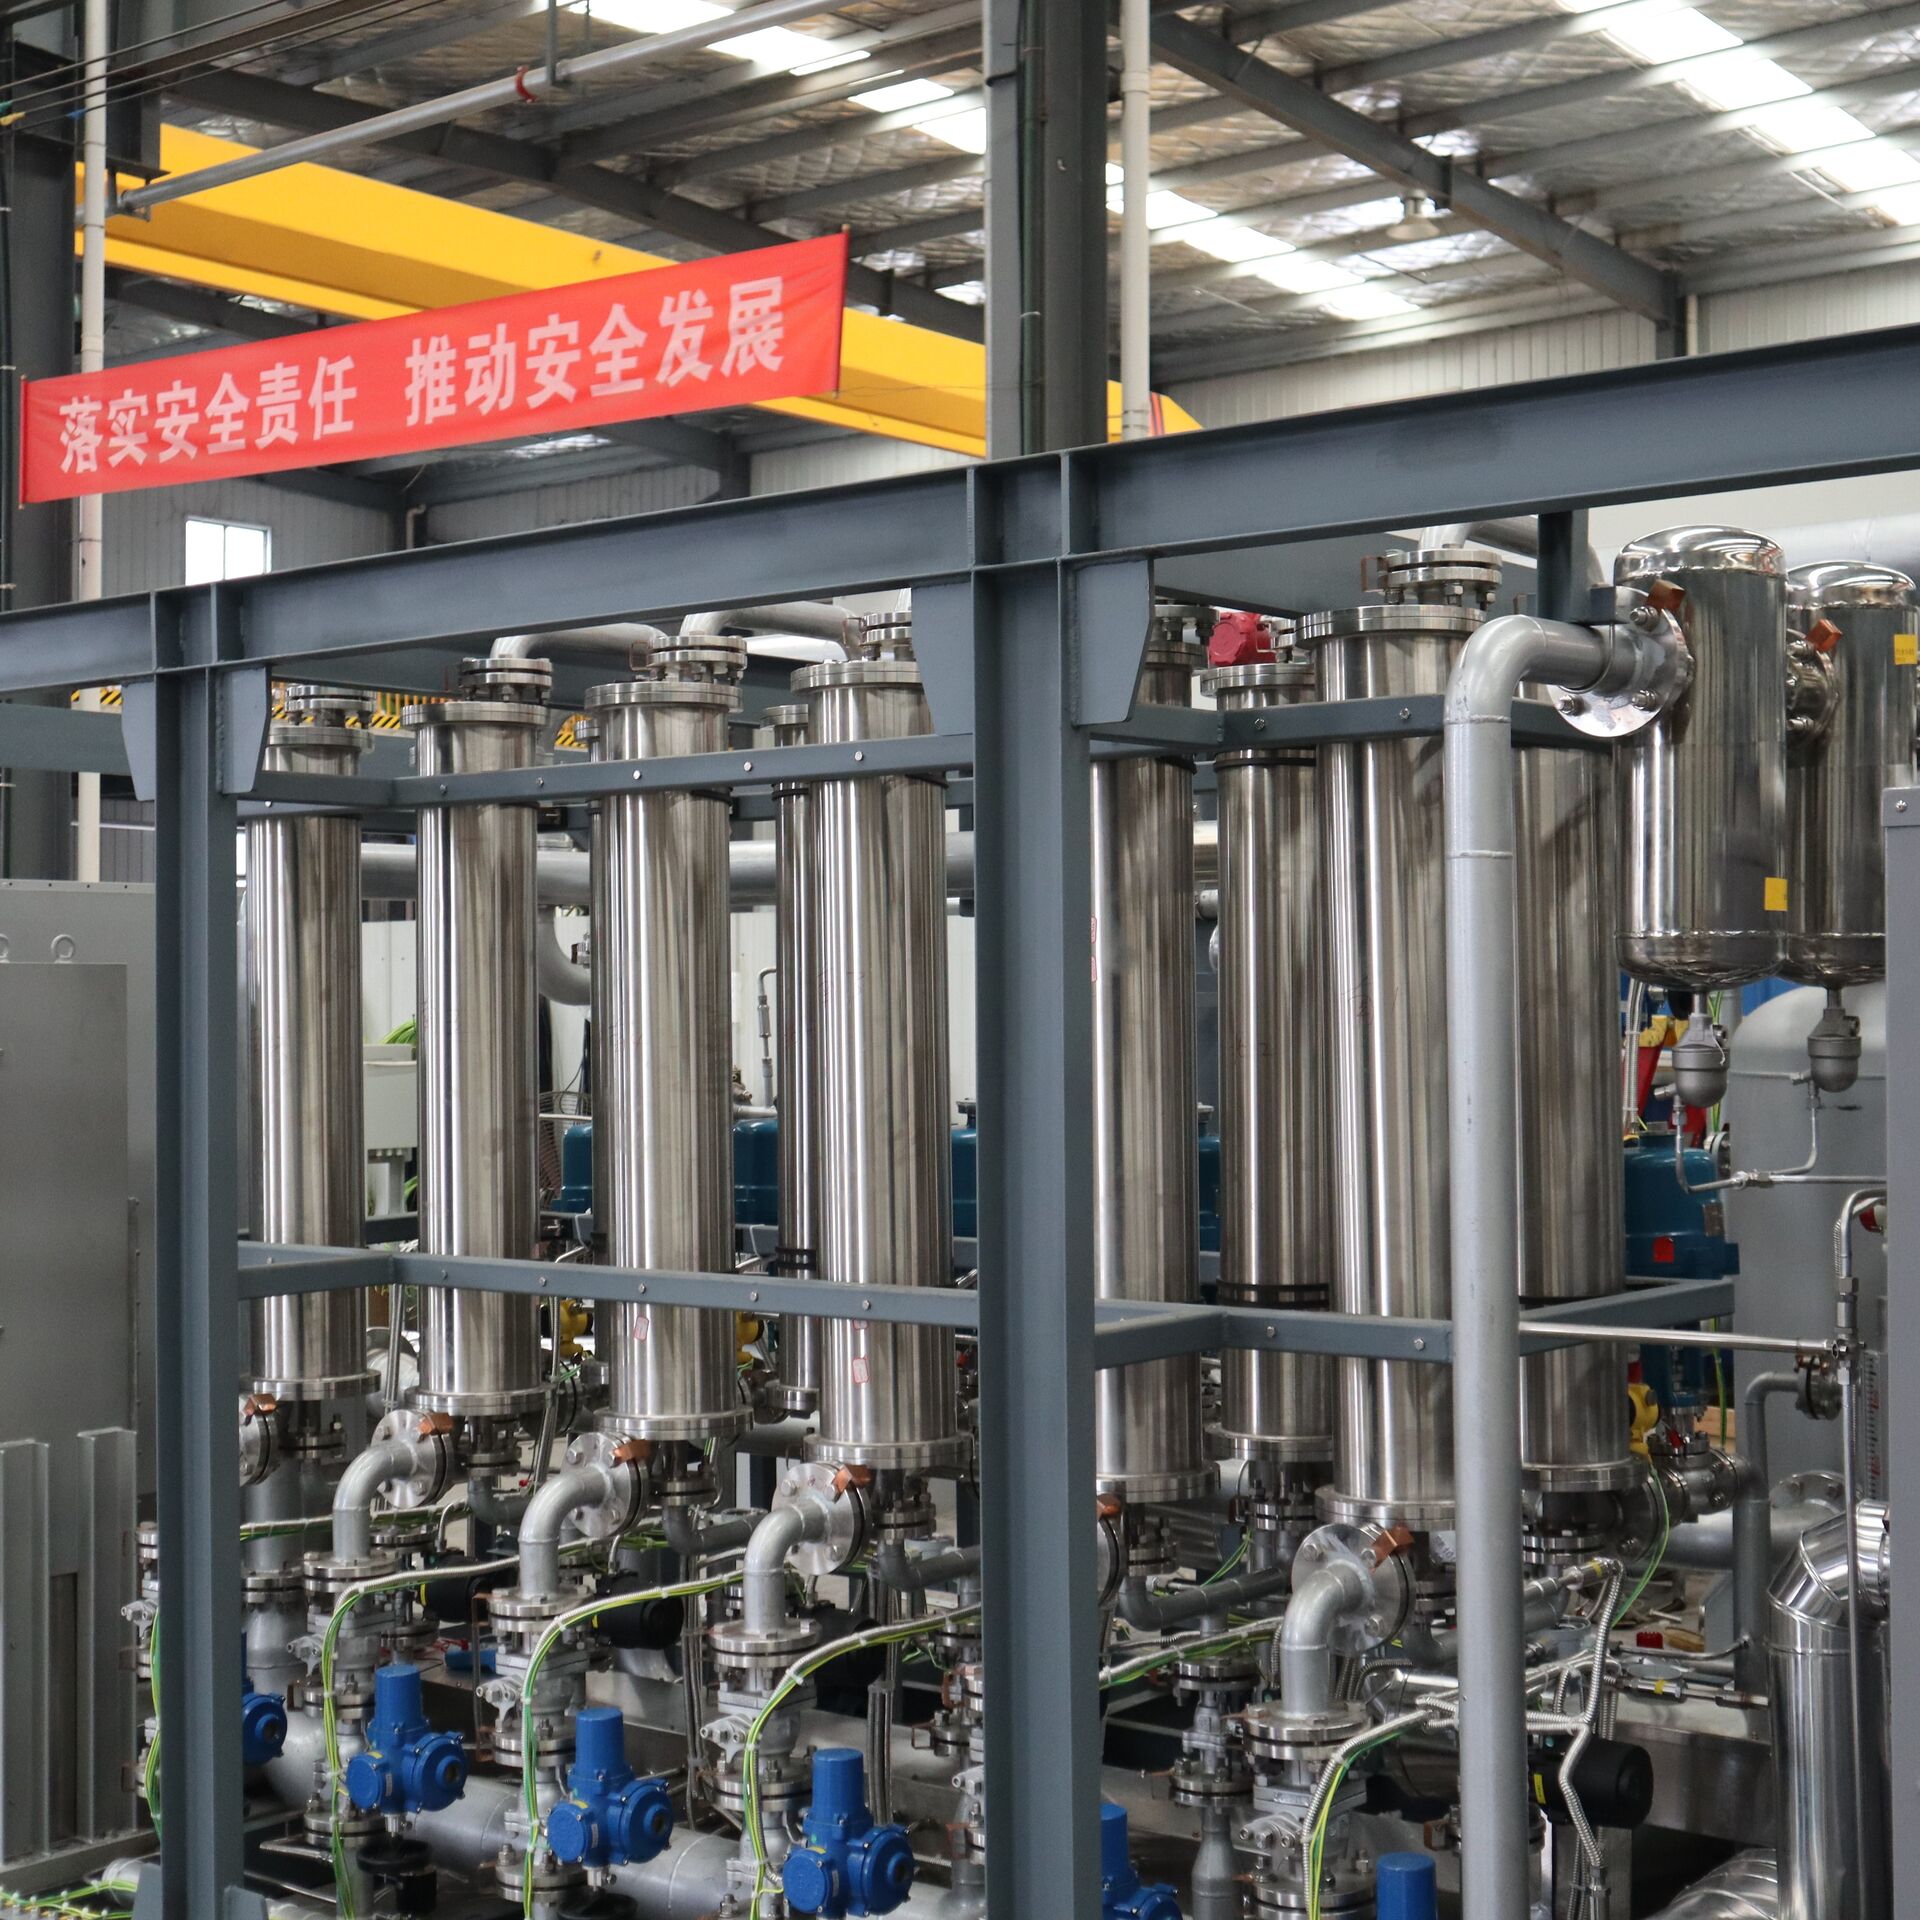
The service life of the core consumables membrane module is three to five years. The daily maintenance is mainly to check the pressure and recovery liquid level of the refrigeration system every week, clean the heat exchanger fins every month, and replace the freezing oil and drying filter every year. There is no frequent replacement of consumables. Trouble.
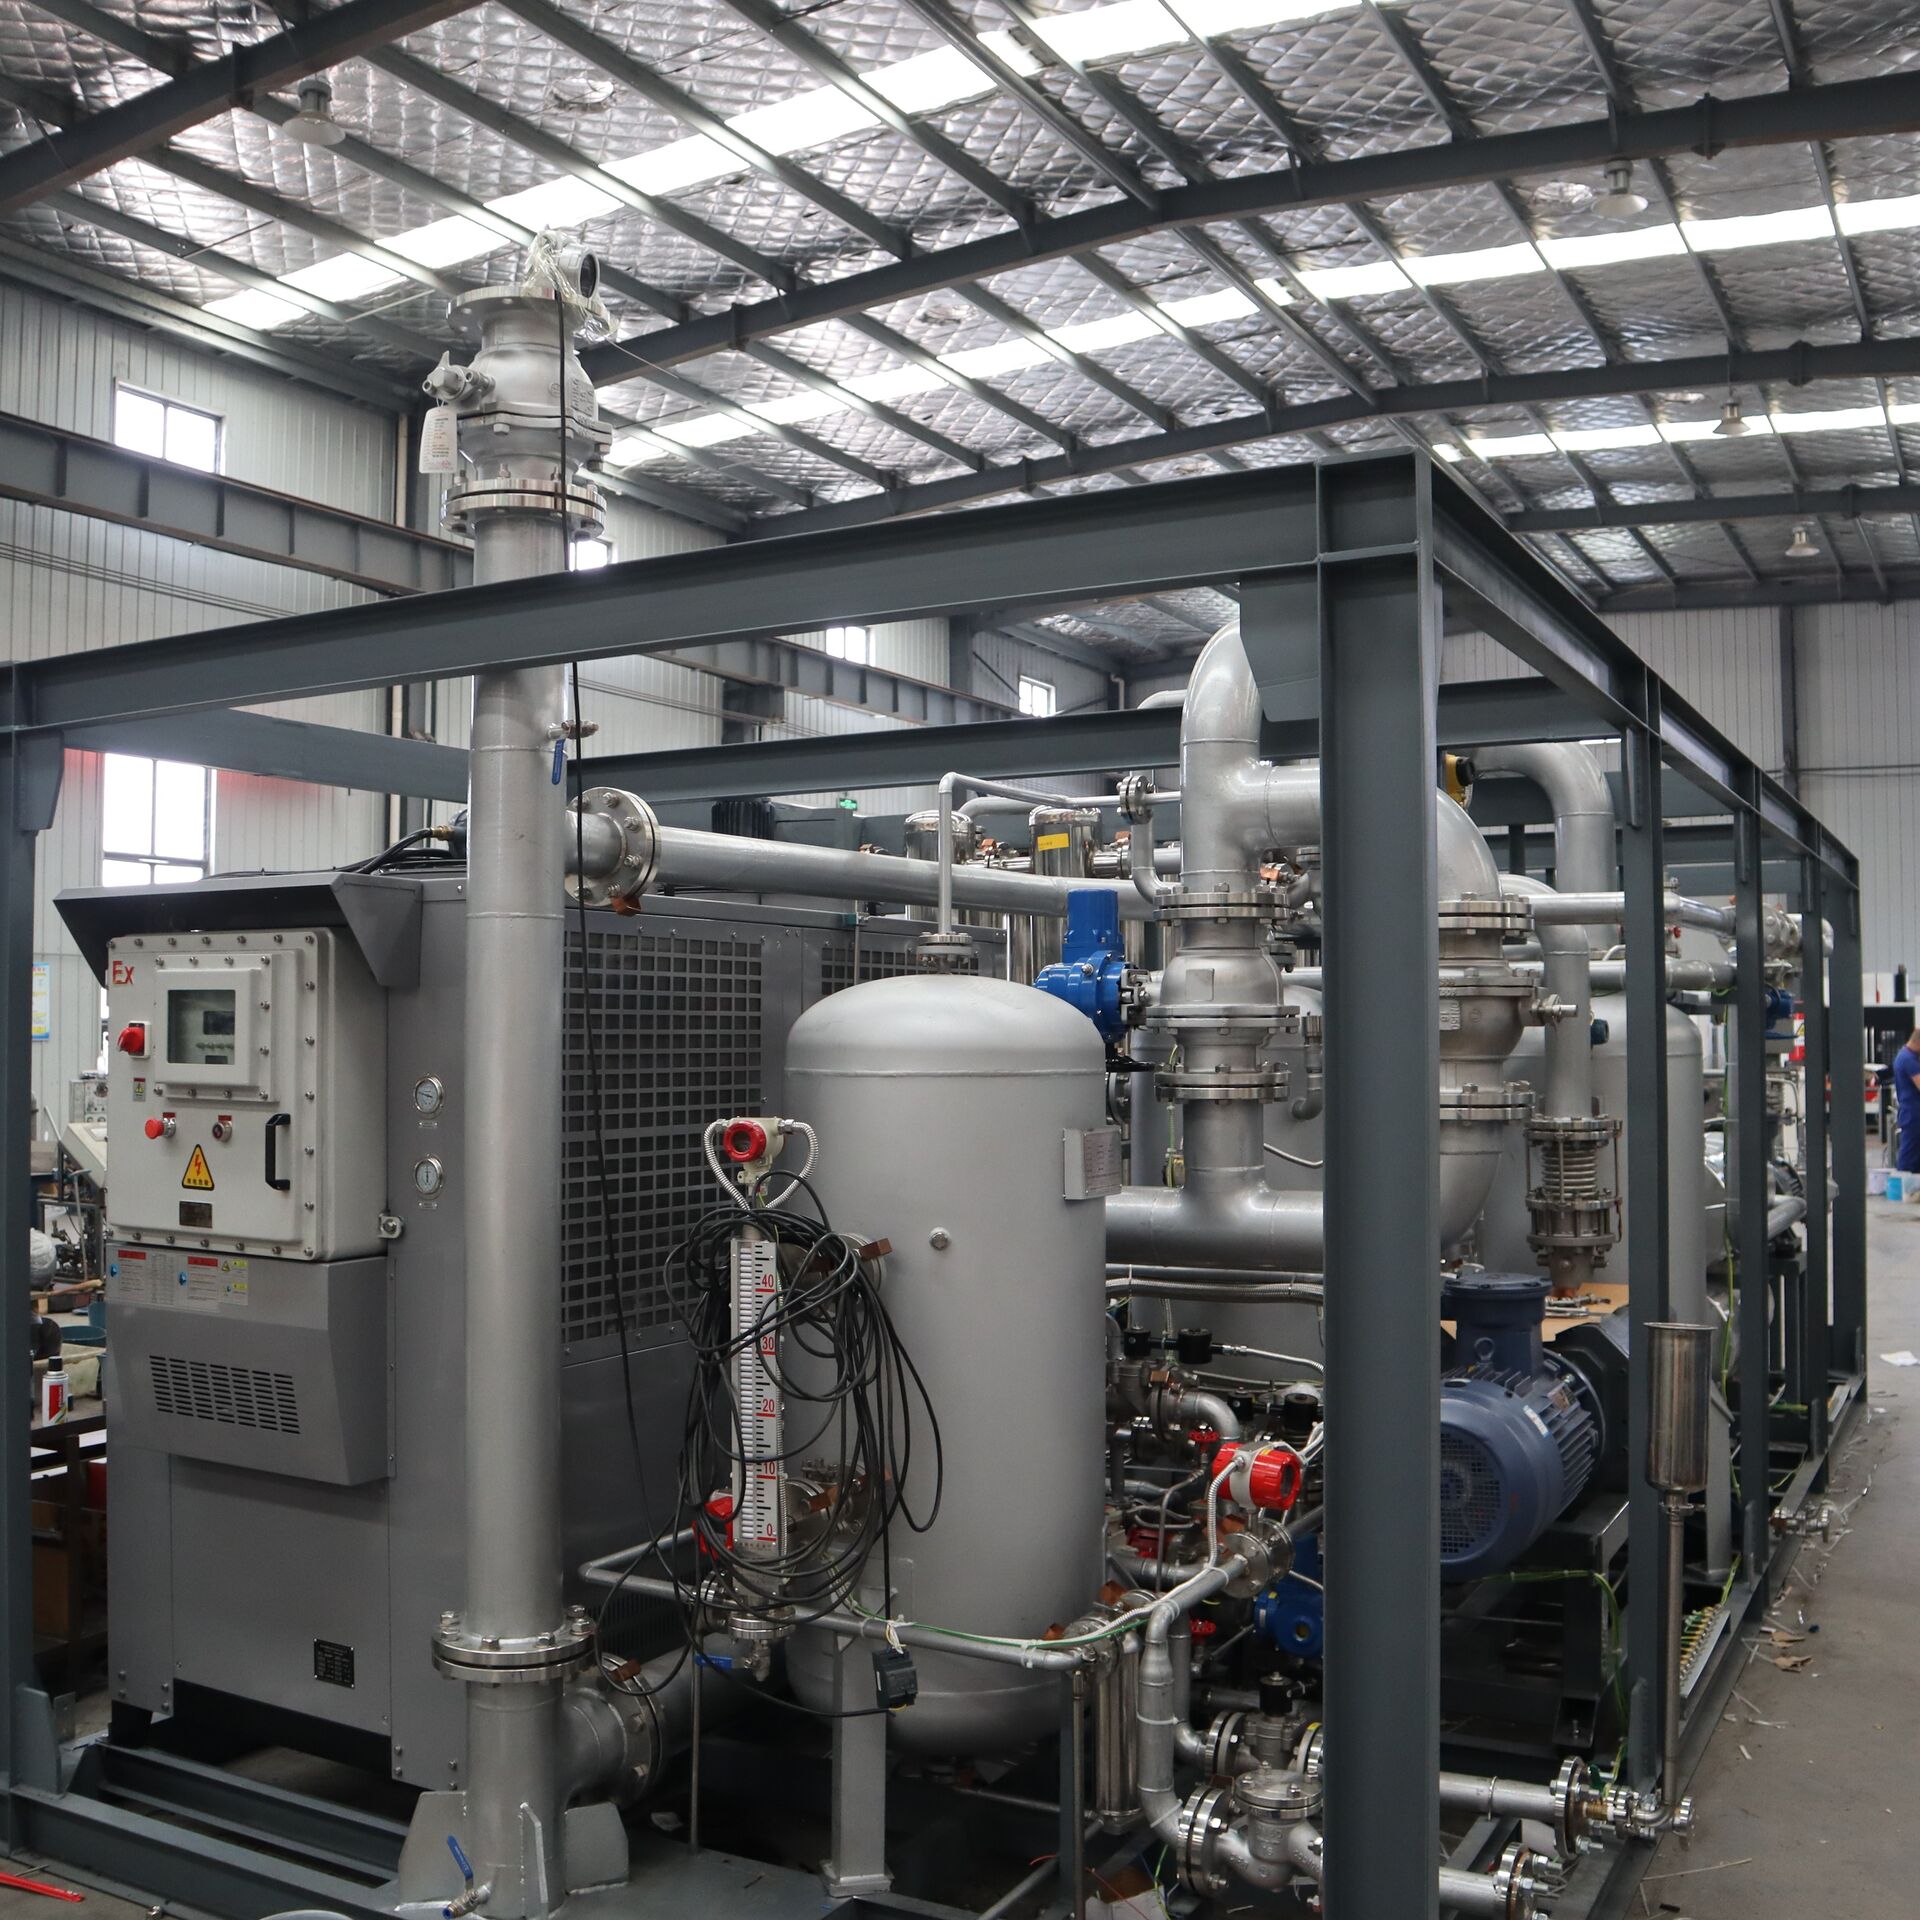
All parts of the equipment are integrated on a stainless steel base, and assembled and tested before leaving the factory. The site can be used only by connecting the power source and air duct. The installation period is short, the floor area is small, and the explosion-proof configuration is optional, which is suitable for explosion-proof places such as pharmaceuticals.
The equipment has good recovery effect on common organic solvents such as hydrocarbons, esters, ketones, alcohols, halogenated hydrocarbons, etc., and is suitable for medium and high concentration exhaust gas treatment in pharmaceutical, chemical, printing, coating, electronics, gas stations and other industries. Scenarios can also be customized according to customer working conditions.
Relying on the R & D platform of Henan Oil and Gas Recovery Engineering Technology Research Center, Luoyang Wo Hong Petrochemical Equipment Co., Ltd. has set up a professional scientific research, manufacturing and marketing team, which can provide customers with complete support from the early stage to the late stage. In the early stage, free working condition investigation and exhaust gas composition analysis will be provided, and targeted technical plans and payback period calculation will be issued. In the medium term, responsible for equipment manufacturing, factory testing, transportation, installation guidance, debugging and operator training; In the later period, one-year warranty, spare parts supply, remote technical support and regular inspection services will be provided. Customers can also sign long-term maintenance contracts as required.
In the field of organic waste gas treatment in the pharmaceutical industry, membrane condensation technology has become an ideal choice for many enterprises with its significant advantages. Luoyang Wo Hong Petrochemical Equipment Co., Ltd. continues to explore and innovate in this field, providing enterprises with high-quality products and services, and helping enterprises to achieve green and sustainable development.
Mr. Li 13526990215

Hotline





