
In the pharmaceutical industry, solvent recovery has always been a highly concerned topic. During the pharmaceutical process, a large amount of waste gas containing organic solvents is generated, which not only pollutes the environment but also causes waste of resources. Therefore, solvent recovery is particularly necessary. So, how to efficiently and economically recover solvents? Membrane condensation recovery equipment may be a good choice.
traditionalwaste gas treatmentThere are many pain points in the way. For example, many companies useactivated charcoalThe equipment deals with exhaust gas, and the activated carbon needs to be replaced frequently, once a month. The cost of replacing carbon is high, and the replaced waste carbon is hazardous waste, with complicated processing procedures and high labor costs. Meanwhile, activated carbon adsorption only transfers organic matter from exhaust gas to carbon, and does not truly solve the problem of exhaust gas pollution. Besides,RTOAlthough the equipment has a good effect on treating exhaust gas, the operating cost is high, especially when dealing with low concentration exhaust gas. The gas cost is high, and the burned gas has a higher value than the recovered solvent. If the operating load is reduced and the emissions do not meet the standards, it is a pity that the solvent in the exhaust gas is burned off.
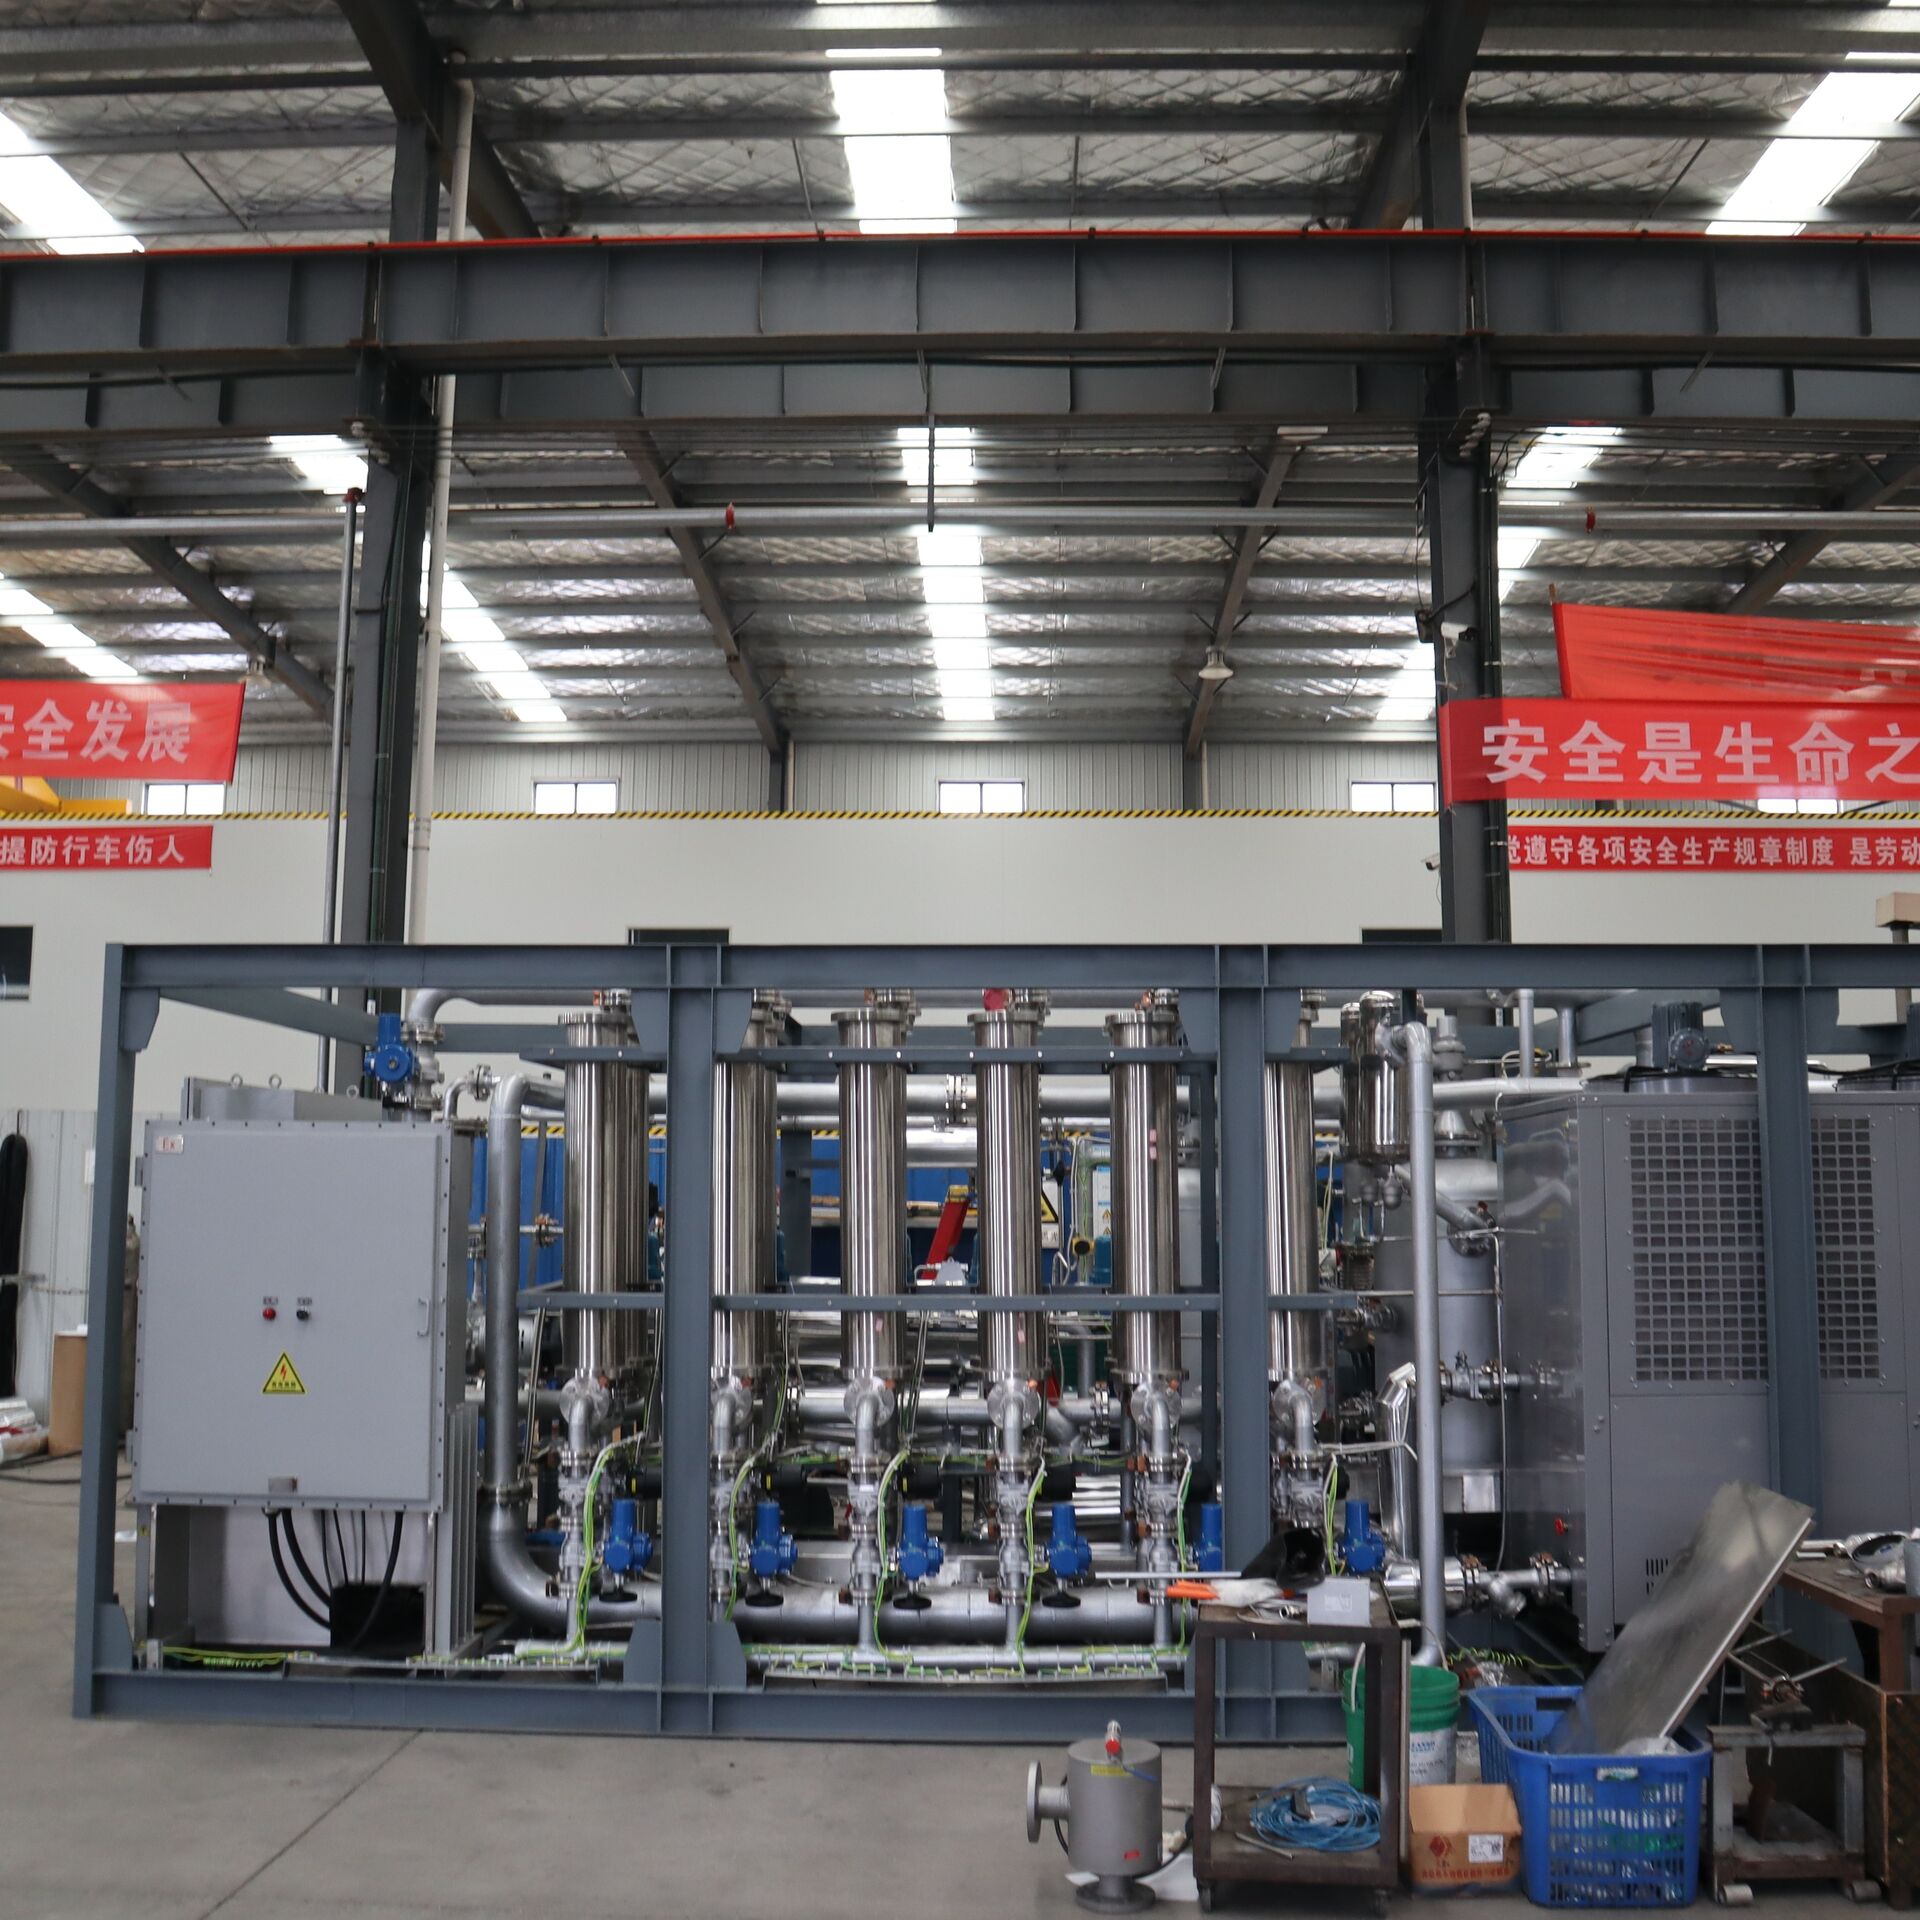
The membrane condensation recovery equipment can effectively solve these problems. In LuoyangWohong PetrochemicalTaking the membrane condensation recovery unit of Equipment Co., Ltd. as an example, it adopts a three-stage condensation processgas separation membraneCombination process, suitable for the treatment of medium to high concentration organic waste gases in industries such as chemical, pharmaceutical, and gas stations.
From the perspective of operating costs, the equipment only uses electricity and does not burn gas. The refrigeration compressor and vacuum pump are both controlled by frequency conversion, which can automatically adjust the power according to the exhaust gas load, effectively controlling power consumption and greatly reducing operating costs. In terms of solvent recovery, the equipment can condense and liquefy organic solvents in exhaust gas for recovery, with a purity of over 90%. The recovered solvents can be directly reused for production or external sales, converting environmental protection expenses into economic benefits.
In terms of maintenance, the service life of the core consumable membrane components is three to five years. Daily maintenance mainly involves checking the pressure and recovery liquid level of the refrigeration system every week, cleaning the heat exchanger fins every month, and replacing the refrigeration oil and drying filter every year, without the hassle of frequent consumables replacement.
This device adopts a modular integrated design, with all components integrated on a stainless steel base. It is assembled and tested before leaving the factory, and can be used on site by simply connecting the power supply and air duct. The installation cycle is short, the footprint is small, and there is also an optional explosion-proof configuration, suitable for explosion-proof places such as chemical and pharmaceutical industries. In addition, it has good recovery effects on common organic solvents such as hydrocarbons, esters, ketones, alcohols, and halogenated hydrocarbons, and has a wide range of applications. It can also be customized according to customer working conditions.
Luoyang Wohong Petrochemical Equipment Co., Ltd. has established a professional research, manufacturing, and marketing team based on the R&D platform of Henan Oil and Gas Recovery Engineering Technology Research Center, and designed various technical solutions and equipment for VOCs waste gas recovery and treatment. The company can provide complete support from the early stage to the later stage, conducting free working condition research and exhaust gas composition analysis in the early stage, and issuing targeted technical solutions and investment payback period calculations; In the mid-term, responsible for equipment manufacturing, testing, transportation, installation guidance, etc; Provide one-year warranty, spare parts supply and other services in the later stage.
On the issue of solvent recovery in the pharmaceutical industry, membrane condensation recovery equipment stands out with its significant advantages, and the professional ability and high-quality service of Luoyang Wo Hong Petrochemical Equipment Co., Ltd. in this field also provides a reliable choice for enterprises to solve the problems of waste gas treatment and solvent recovery.
Mr. Li 13526990215

Hotline





