
In the chemical industry, the treatment of high concentrations of VOCs (volatile organic compounds) has always been a challenge. Not only will it cause serious pollution to the environment, but it may also pose a threat to human health. Therefore, choosing appropriate processing equipment is crucial, and membrane condensation recovery equipment has become the first choice for many enterprises. So, how to select membrane condensation equipment? Below is a detailed analysis for everyone.
Before choosing a membrane condensation equipment, it is necessary to first understand the three core parameters of the exhaust gas: concentration, air volume, and composition. The concentration affects the processing capacity and recovery efficiency of the equipment; The air volume determines the processing scale of the equipment; And the composition is related to the applicability and recycling effect of the equipment. Different organic solvents, such as hydrocarbons, esters, ketones, alcohols, halogenated hydrocarbons, etc., also have different requirements for equipment.
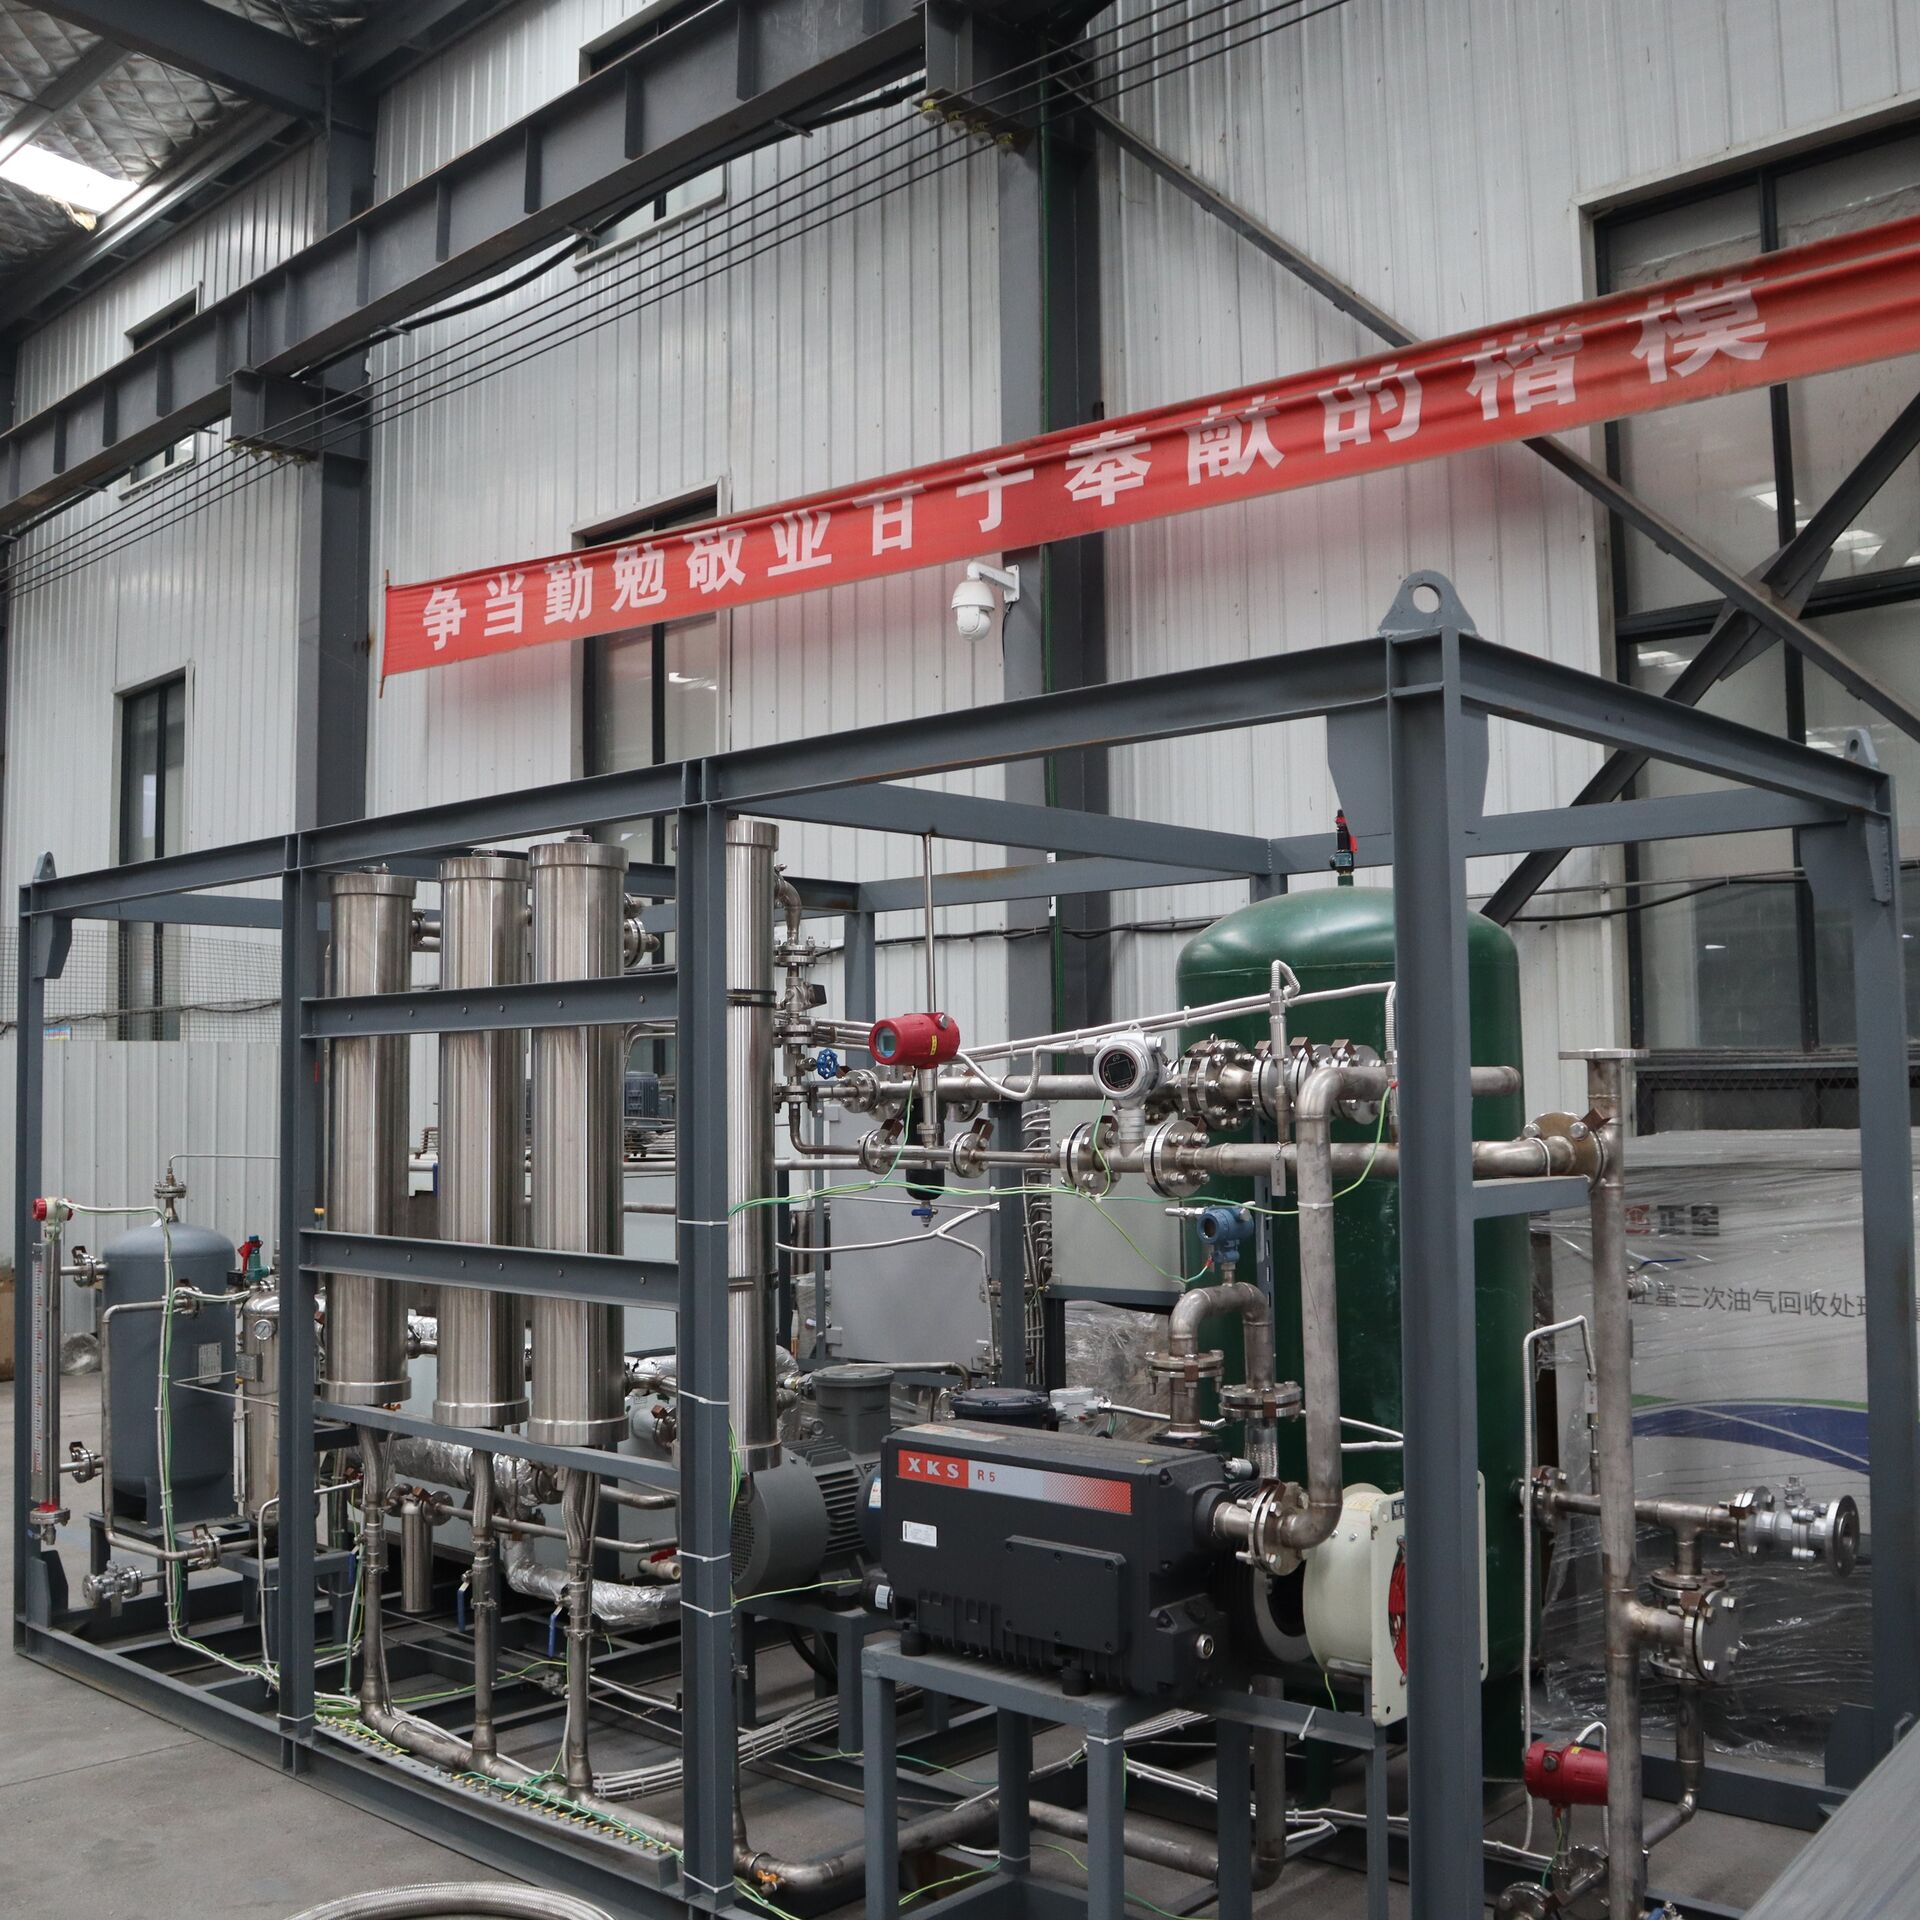
Membrane condensation recovery equipment adopts three-stage condensation plusgas separation membraneCombination technology has many advantages. Firstly, the operating cost is low, and the equipment only consumes electricity. The refrigeration compressor and vacuum pump are both controlled by frequency conversion, which can automatically adjust the power according to the exhaust gas load, effectively controlling power consumption. Secondly, solvent recovery can generate revenue by condensing and liquefying organic solvents in exhaust gas, achieving a high level of purity. The recovered solvents can be directly reused for production or external sales, converting environmental expenses into economic benefits. Furthermore, the frequency of consumable replacement is low, the service life of core consumable membrane components is long, and daily maintenance is relatively simple, without the hassle of frequent consumable replacement. In addition, the integrated design of the pry and install allows all components of the equipment to be integrated on a stainless steel base, which is assembled and tested before leaving the factory. On site, only the power and air ducts need to be connected for use, with a short installation cycle, small footprint, and optional explosion-proof configuration, suitable for explosion-proof places such as chemical and pharmaceutical industries.
Compared with traditional processing methods, membrane condensation equipment has significant advantages. For exampleactivated charcoalAdsorption, many companies use activated carbon equipment, but the cost of replacing carbon is high and the procedures are cumbersome. Moreover, activated carbon adsorption only transfers organic matter from exhaust gas to carbon, and the problem has not been truly solved. AlsoRTOThe equipment has a good effect on treating exhaust gas, but the gas consumption is high, especially when dealing with low concentration exhaust gas. The operating cost is unbearable, and it is a pity that the solvents in the exhaust gas are burned off. And membrane condensation equipment can effectively avoid these problems.
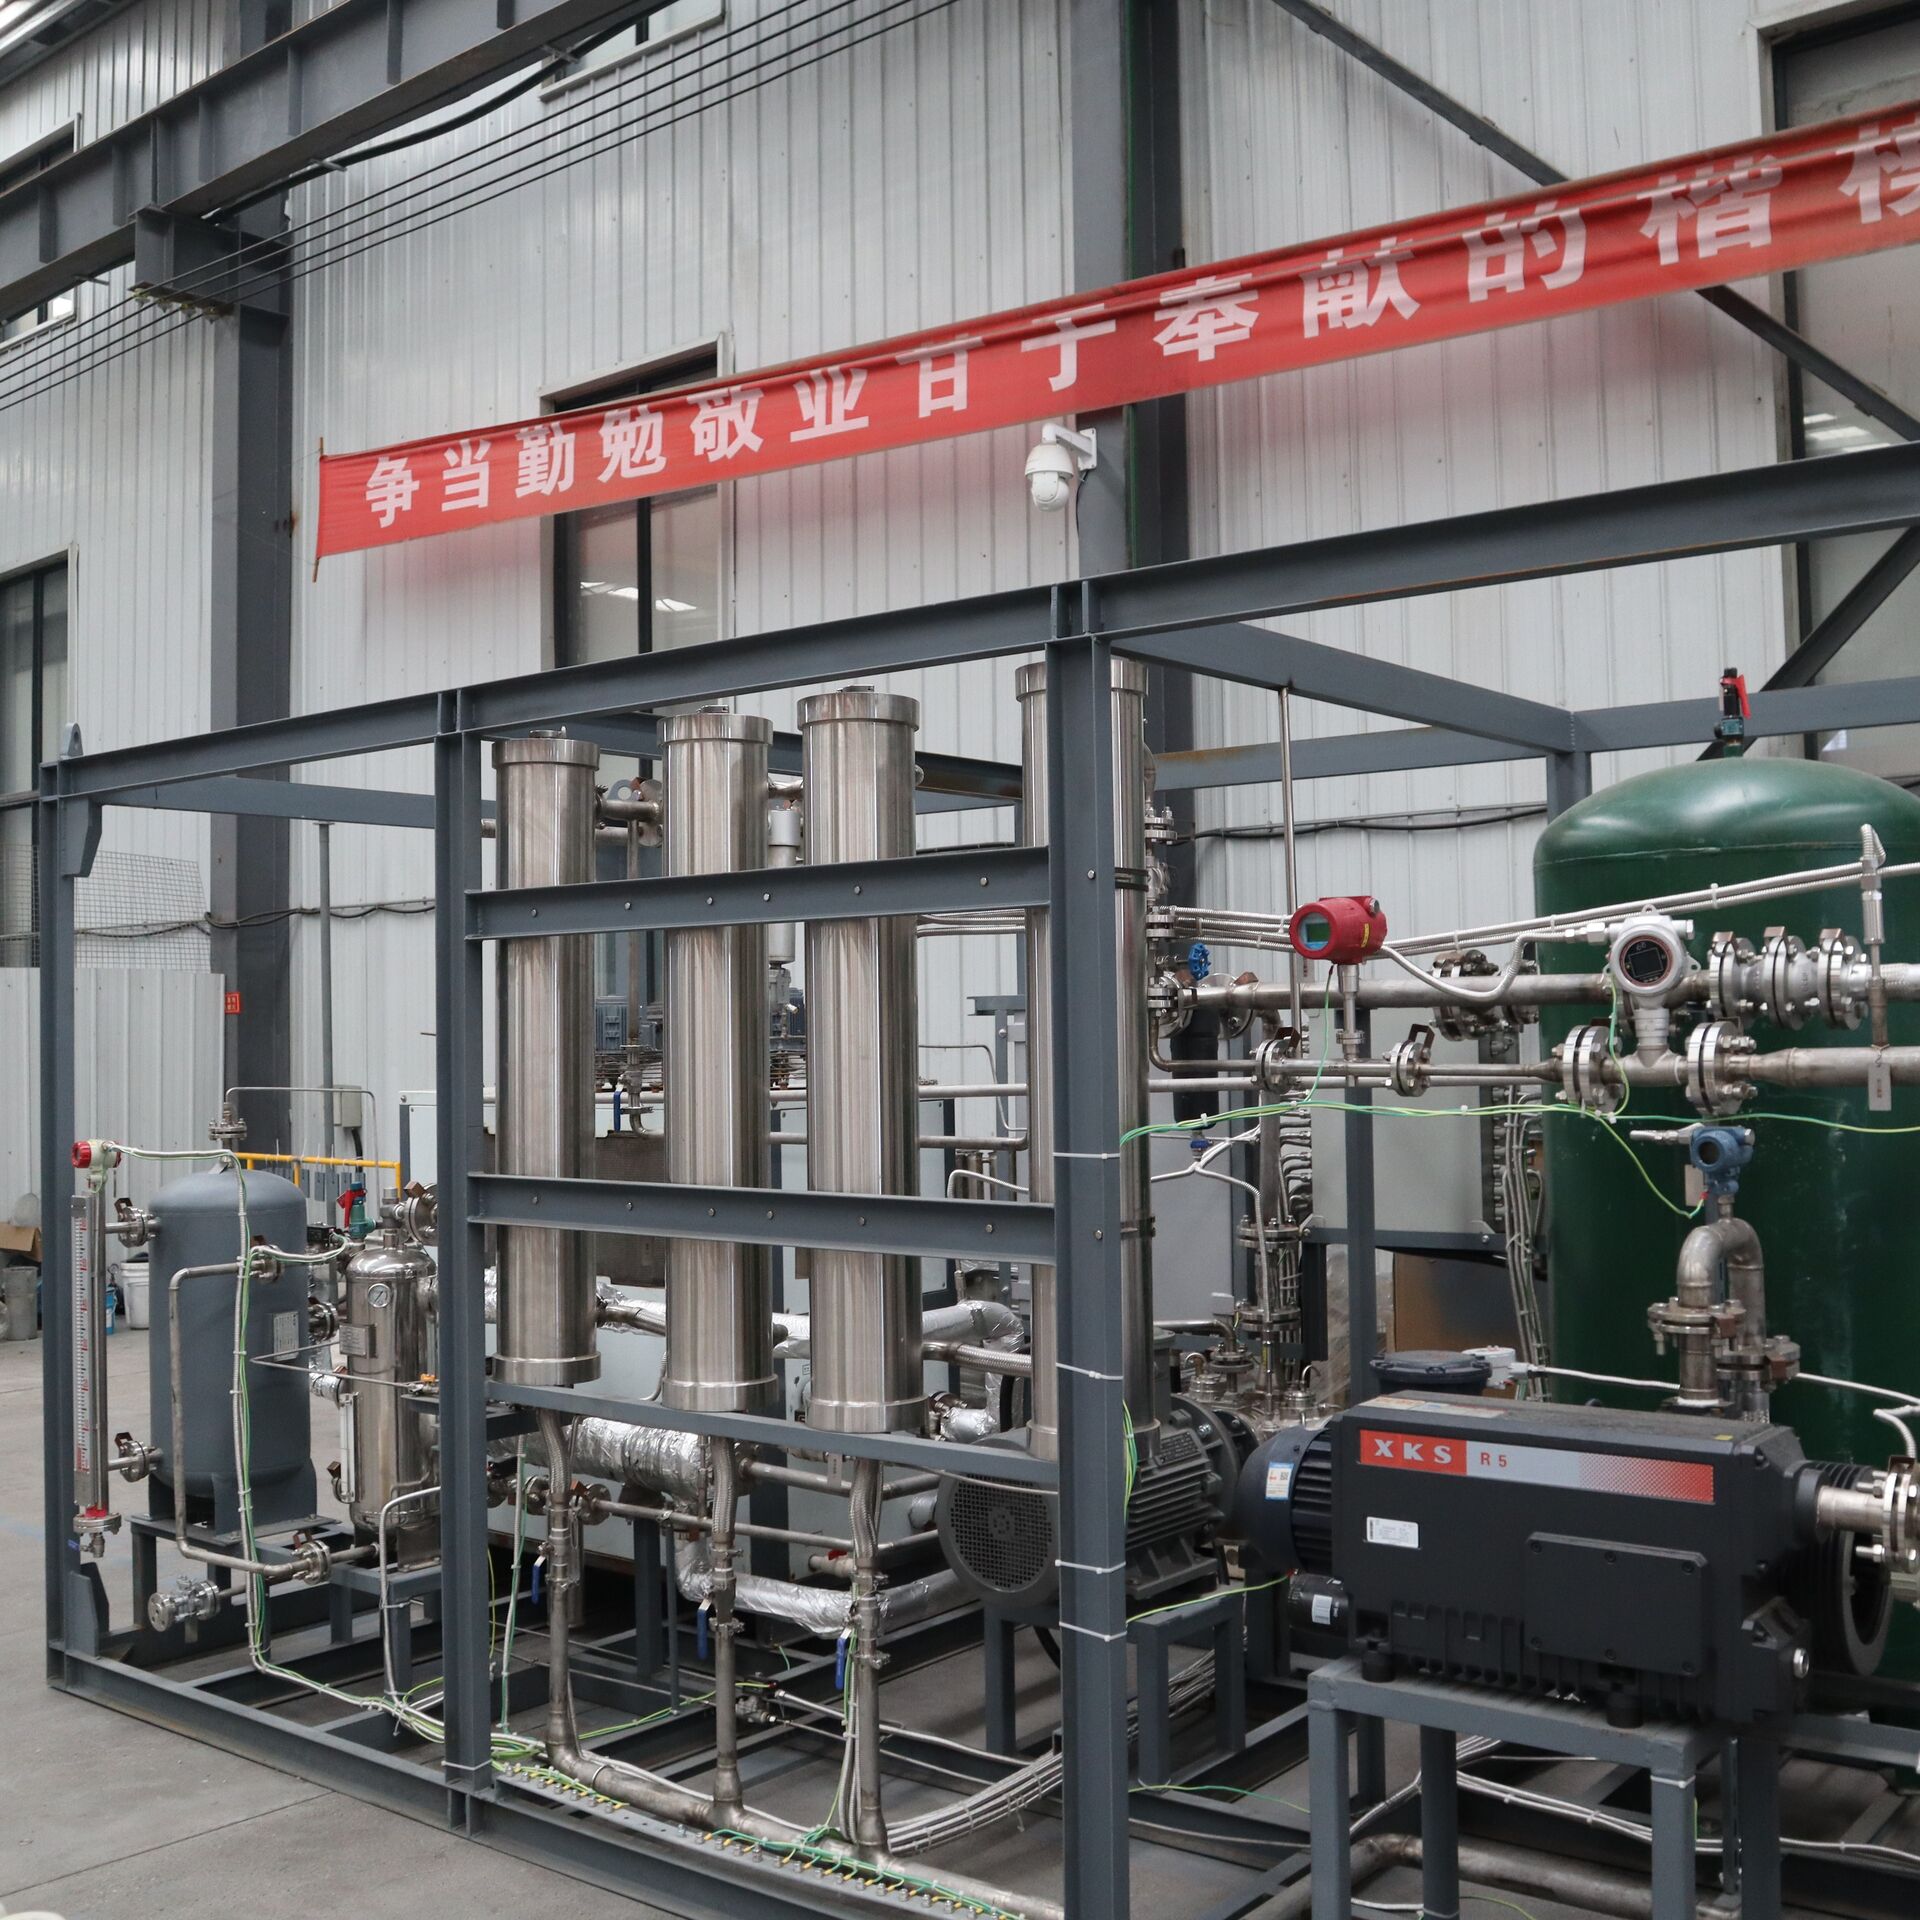
When selecting equipment, it is necessary to take into account the actual working conditions of the enterprise, combined with parameters such as VOCs concentration, air volume, and composition, to choose equipment with appropriate air processing volume that can meet the recycling requirements. At the same time, the customizability of the equipment should be considered to ensure that it can adapt to different working conditions. In addition, attention should be paid to the service capabilities of equipment suppliers, including free working condition research and exhaust gas composition analysis in the early stage, equipment manufacturing and installation debugging in the middle stage, and quality assurance and maintenance services in the later stage.
LuoyangWohong PetrochemicalEquipment Co., Ltd. focuses on the field of VOC waste gas treatment and has rich experience in the research and development, manufacturing, sales, and supporting services of membrane condensation recovery equipment. The company has a complete membrane module production line and condensation equipment manufacturing workshop, with full process service capabilities from working condition analysis to equipment delivery. It can provide customized solutions for customers and is a reliable choice for chemical enterprises to handle high concentration VOCs.
Mr. Li 13526990215

Hotline





