
Ethanol is used in fermentation, pharmaceutical, chemical and disinfection products industries. The concentration of ethanol in the tail gas is high, the gas is large, and the recovery economy is generally good. However, the boiling point of ethanol is about 78 ℃ and it is completely miscible with water. These two properties determine that its recovery configuration cannot copy the set of toluene and xylene: the condensation temperature should be lower, and the recovered liquid will almost necessarily carry water and need to be treated before reuse.
Ethanol tail gas in the fermentation industry is concentrated in the fermentation tank breathing and tank, distillation tower top non-condensable gas, as well as preparation and filling links. Fermentation tank respiration is a continuous low concentration discharge, distillation link is a high concentration of concentrated discharge, the concentration difference between the two gases is very large, the treatment should be considered separately. Ethanol tail gas in the chemical industry mostly comes from reaction tail gas, tank breathing and cleaning operations.
Although the concentration of breath gas in the fermentation tank is not high, it has a large amount of gas and a long duration. The accumulated ethanol loss throughout the year is considerable, and it is a gas whose recovery value cannot be ignored.
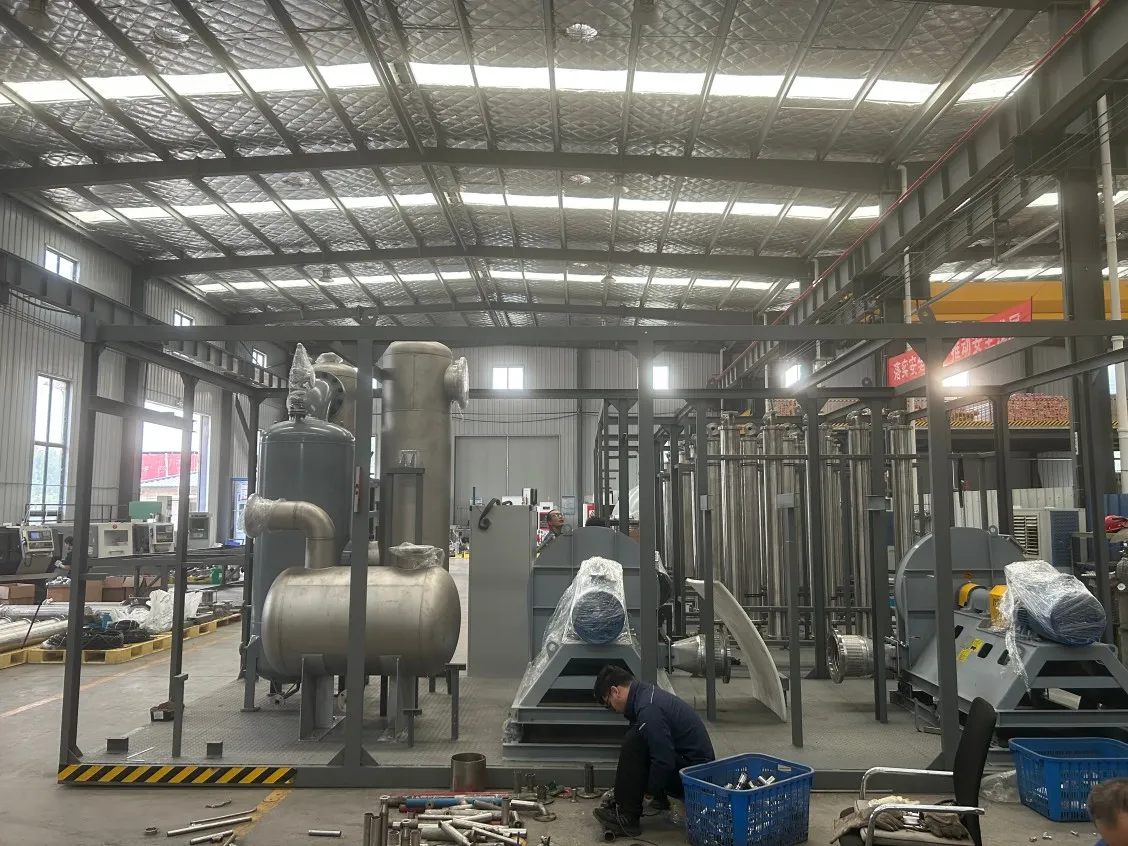
The breathing port and exhaust port of the fermentation tank receive the manifold. When multiple tanks are connected to the main pipe, the air valve is set according to the batch start and stop of the tank to avoid empty tank suction. The concentration of non-condensable gas at the top of the distillation tower is high, which is recovered separately and not combined with low-concentration gas flow. The tank breathing port is equipped with a collection interface, and the displacement gas during loading and unloading operations is collected together.
The slope of the collection pipeline and the liquid collection point should be set in place: the amount of ethanol vapor condensed on the pipe wall is larger than that of aromatic hydrocarbons, the liquid accumulation in the pipeline is more common than other solvents, and the low-point liquid discharge should be a daily inspection item.
According to the boiling point of ethanol, the temperature level of the condensing section is one level lower than that of the recovered aromatic hydrocarbons. The high-concentration air stream is pre-cooled to condense water vapor and some ethanol, and then enters the low-temperature section, which can significantly slow down frosting. Breathing gas with low concentration and large flow should be increased or graded first, and the energy consumption of direct cryogenic treatment of large flow and low concentration airflow is not cost-effective.
The particularity of mutual solubility with water is that the condensate is a mixture of alcohol and water, and there is no convenience of "oil-water stratification. The treatment depth of the recovered liquid is determined according to the reuse requirements, the threshold for fuel or disinfection is low, and the reuse of chemical raw materials requires distillation and concentration.
| Segment | Configuration considerations | Description |
|---|---|---|
| Breathing of fermentation tank | large flow and low concentration | Start and stop the air valve by batch to avoid suction of empty tank |
| Distilled non-condensable gas | high concentration concentration | Recycle all the way alone, pre-cooling first and then deep cooling. |
| Tank Breathing | Loading and unloading period concentration | Breathing mouthpiece collection interface |
| Condensation temperature level | One level lower than aromatic hydrocarbons | Pre-cooling water removal slows frosting |
| Recovery liquid | alcohol water mixture | Determine the concentration depth according to the reuse requirements. |
| Pipeline | Slope and Low Point Drainage | Ethanol pipe wall condensation large, frequent drainage |
The concentration energy consumption of alcohol-water mixture is directly related to the proportion of alcohol: the higher the concentration, the lower the energy consumption of the same index. Therefore, it is more economical to increase the collection concentration and avoid the mixing of high-humidity air flow than to increase the distillation capacity at the back end. The temporary storage of the recovered liquid should be closed, the ethanol moisture absorption is strong, and the concentration of the open storage will decrease.
The concentration alone is inconspicuous, but the gas volume is large, the duration is long, and the annual cumulative amount is considerable. Whether the configuration recovery is based on the annual ethanol loss and device investment accounting, most of the large-scale fermentation plant accounting results are established.
The calorific value of water-containing ethanol decreases and generally needs to be concentrated to a certain concentration for fuel use. The specific concentration requirements are related to the end-of-use process, and the concentration depth is determined according to the purpose.
First check the moisture source of the incoming gas, whether it is combined with the high-humidity airflow, and whether the pre-cooling section is normal. After the incoming air dehumidification is in place, the frosting speed will be significantly slowed down, and the cleaning cycle will be lengthened.
This article by LuoyangWohong PetrochemicalEquipment Co., Ltd. arranges that the company provides design, manufacturing and operation and maintenance services for condensation recovery, membrane separation recovery and complete solvent recovery devices for chemical and pharmaceutical enterprises. If you need process evaluation or scheme configuration, please contact and exchange.
Mr. Li 13526990215

Hotline





