
In the increasingly strict environmental requirements, VOC exhaust treatment equipment is crucial for many enterprises. However, there are significant differences in the daily maintenance and consumable replacement cycles of equipment with different processes, which directly affects the maintenance costs of enterprises. Below, we will analyze in detail the situation of VOC exhaust gas treatment equipment with different processes.
Many companies use activated carbon equipment to treat VOC exhaust gases. However, the maintenance issue of activated carbon technology is more prominent, and the frequency of activated carbon replacement is high, about once a month. Moreover, the cost of carbon replacement is not low. Each time the carbon is replaced and hazardous waste is disposed of, the procedures are cumbersome and the labor cost is also high. And activated carbon adsorption only transfers organic matter from exhaust gas to carbon, without truly solving the problem of exhaust gas.
The RTO equipment has a good effect on treating exhaust gas, but the operating cost is relatively high. Especially when dealing with low concentration exhaust gas, it is necessary to continuously supplement natural gas, which consumes a large amount of gas and even burns gas with a higher value than the recovered solvent. If the operating load is reduced, it will be difficult to meet the emission standards.
LuoyangWohong PetrochemicalLtd. focuses on the field of VOC waste gas treatment, its main membrane condensation recovery unit using three-stage condensation plus.gas separation membraneThe combination process has significant advantages in maintenance costs.
This device only consumes electricity, and both the refrigeration compressor and vacuum pump are controlled by frequency conversion, which can automatically adjust the power according to the exhaust gas load and effectively control power consumption.
The equipment can condense and liquefy organic solvents in the exhaust gas for recovery, and the purity of the recovery can reach a high level. The recycled solvents can be directly reused for production or external sales, converting environmental expenses into economic benefits.
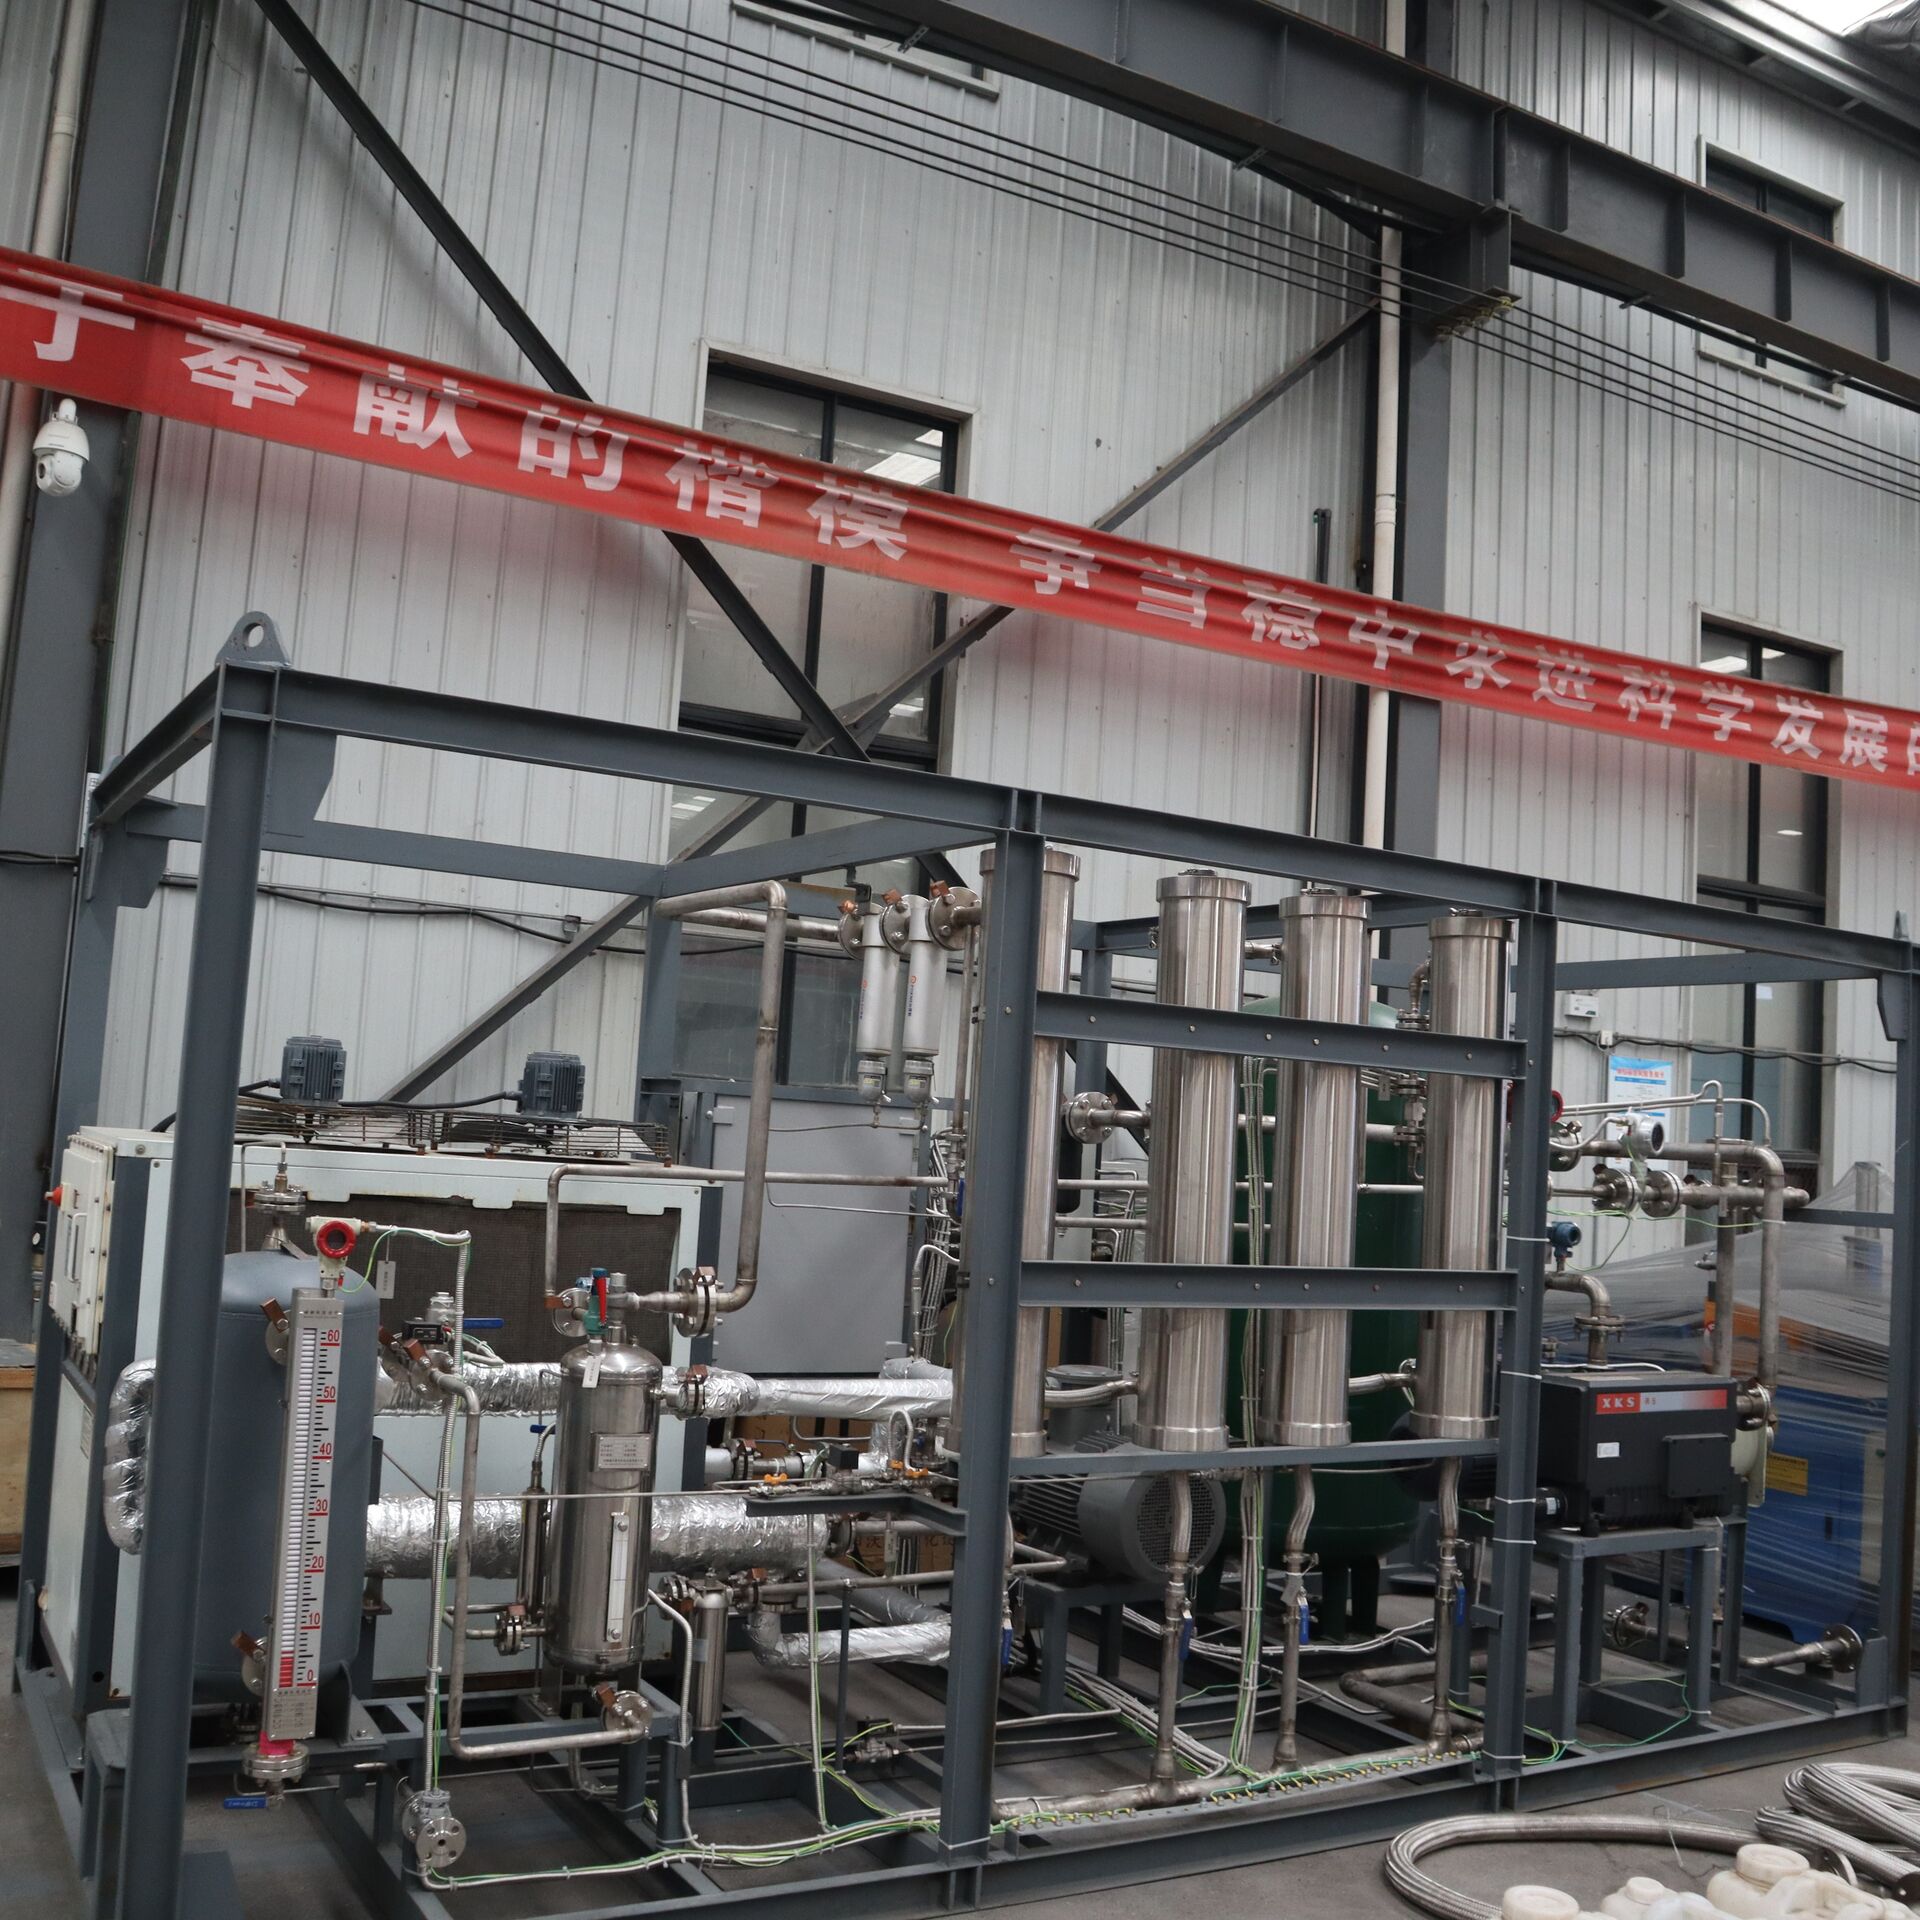
The core consumable membrane module has a service life of three to five years. Daily maintenance is mainly to check the pressure and recovery level of the refrigeration system every week, clean the heat exchanger fins every month, and replace the refrigerating oil and drying filter every year. There is no trouble of frequent replacement of consumables.
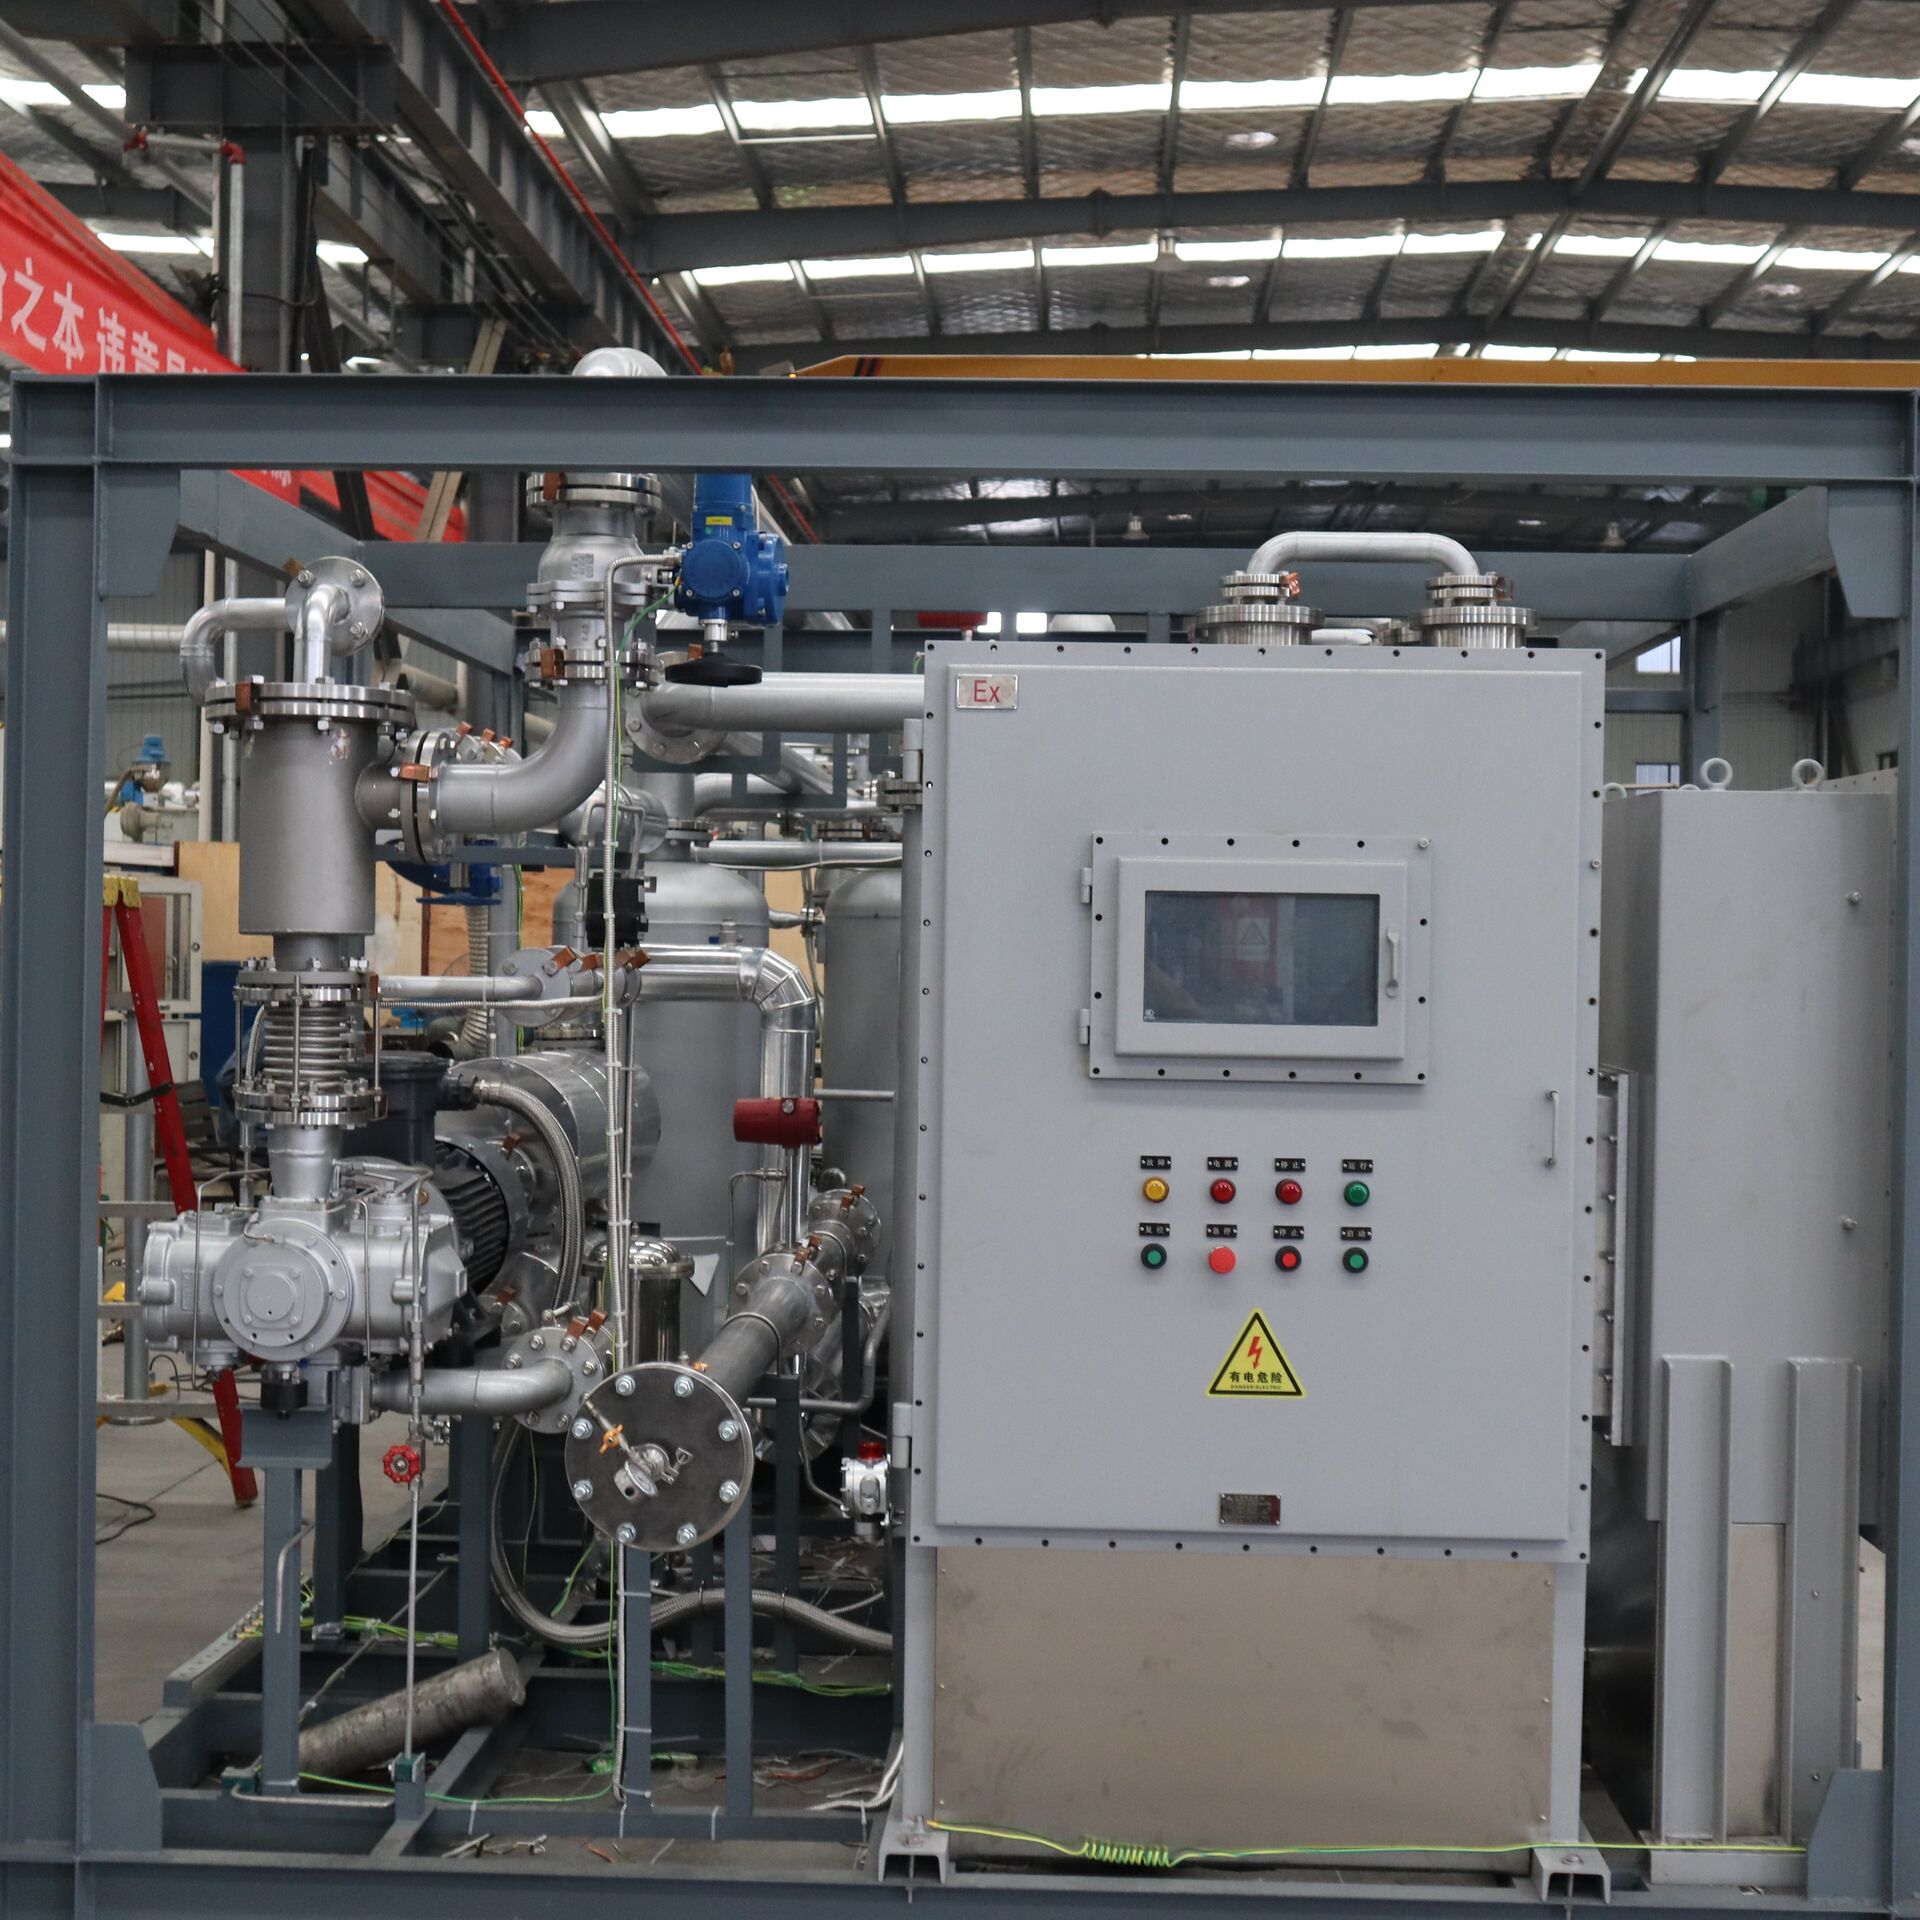
All components of the equipment are integrated on a stainless steel base and assembled and tested before leaving the factory. On site use only requires connecting the power supply and air duct, with a short installation cycle, small footprint, and optional explosion-proof configuration, suitable for explosion-proof places such as chemical and pharmaceutical industries.
The equipment has good recovery effects on common organic solvents such as hydrocarbons, esters, ketones, alcohols, and halogenated hydrocarbons, and is suitable for medium to high concentrations in industries such as chemical, pharmaceutical, printing, coating, electronics, and gas stationswaste gas treatmentScenes can also be customized according to customer conditions.
Luoyang Wohong Petrochemical Equipment Co., Ltd. relies on the R&D platform of Henan Oil and Gas Recovery Engineering Technology Research Center to form a professional team and design various technical solutions and equipment for VOCs waste gas recovery and treatment. This not only effectively reduces harmful gas emissions and protects the ecological environment, but also achieves resource recycling and utilization, helping enterprises achieve green and sustainable development. When choosing VOC exhaust gas treatment equipment, enterprises should comprehensively consider the maintenance costs and effects of different processes. The membrane condensation recovery unit of Luoyang Wohong Petrochemical Equipment Co., Ltd. is worth paying attention to.
Mr. Li 13526990215

Hotline





