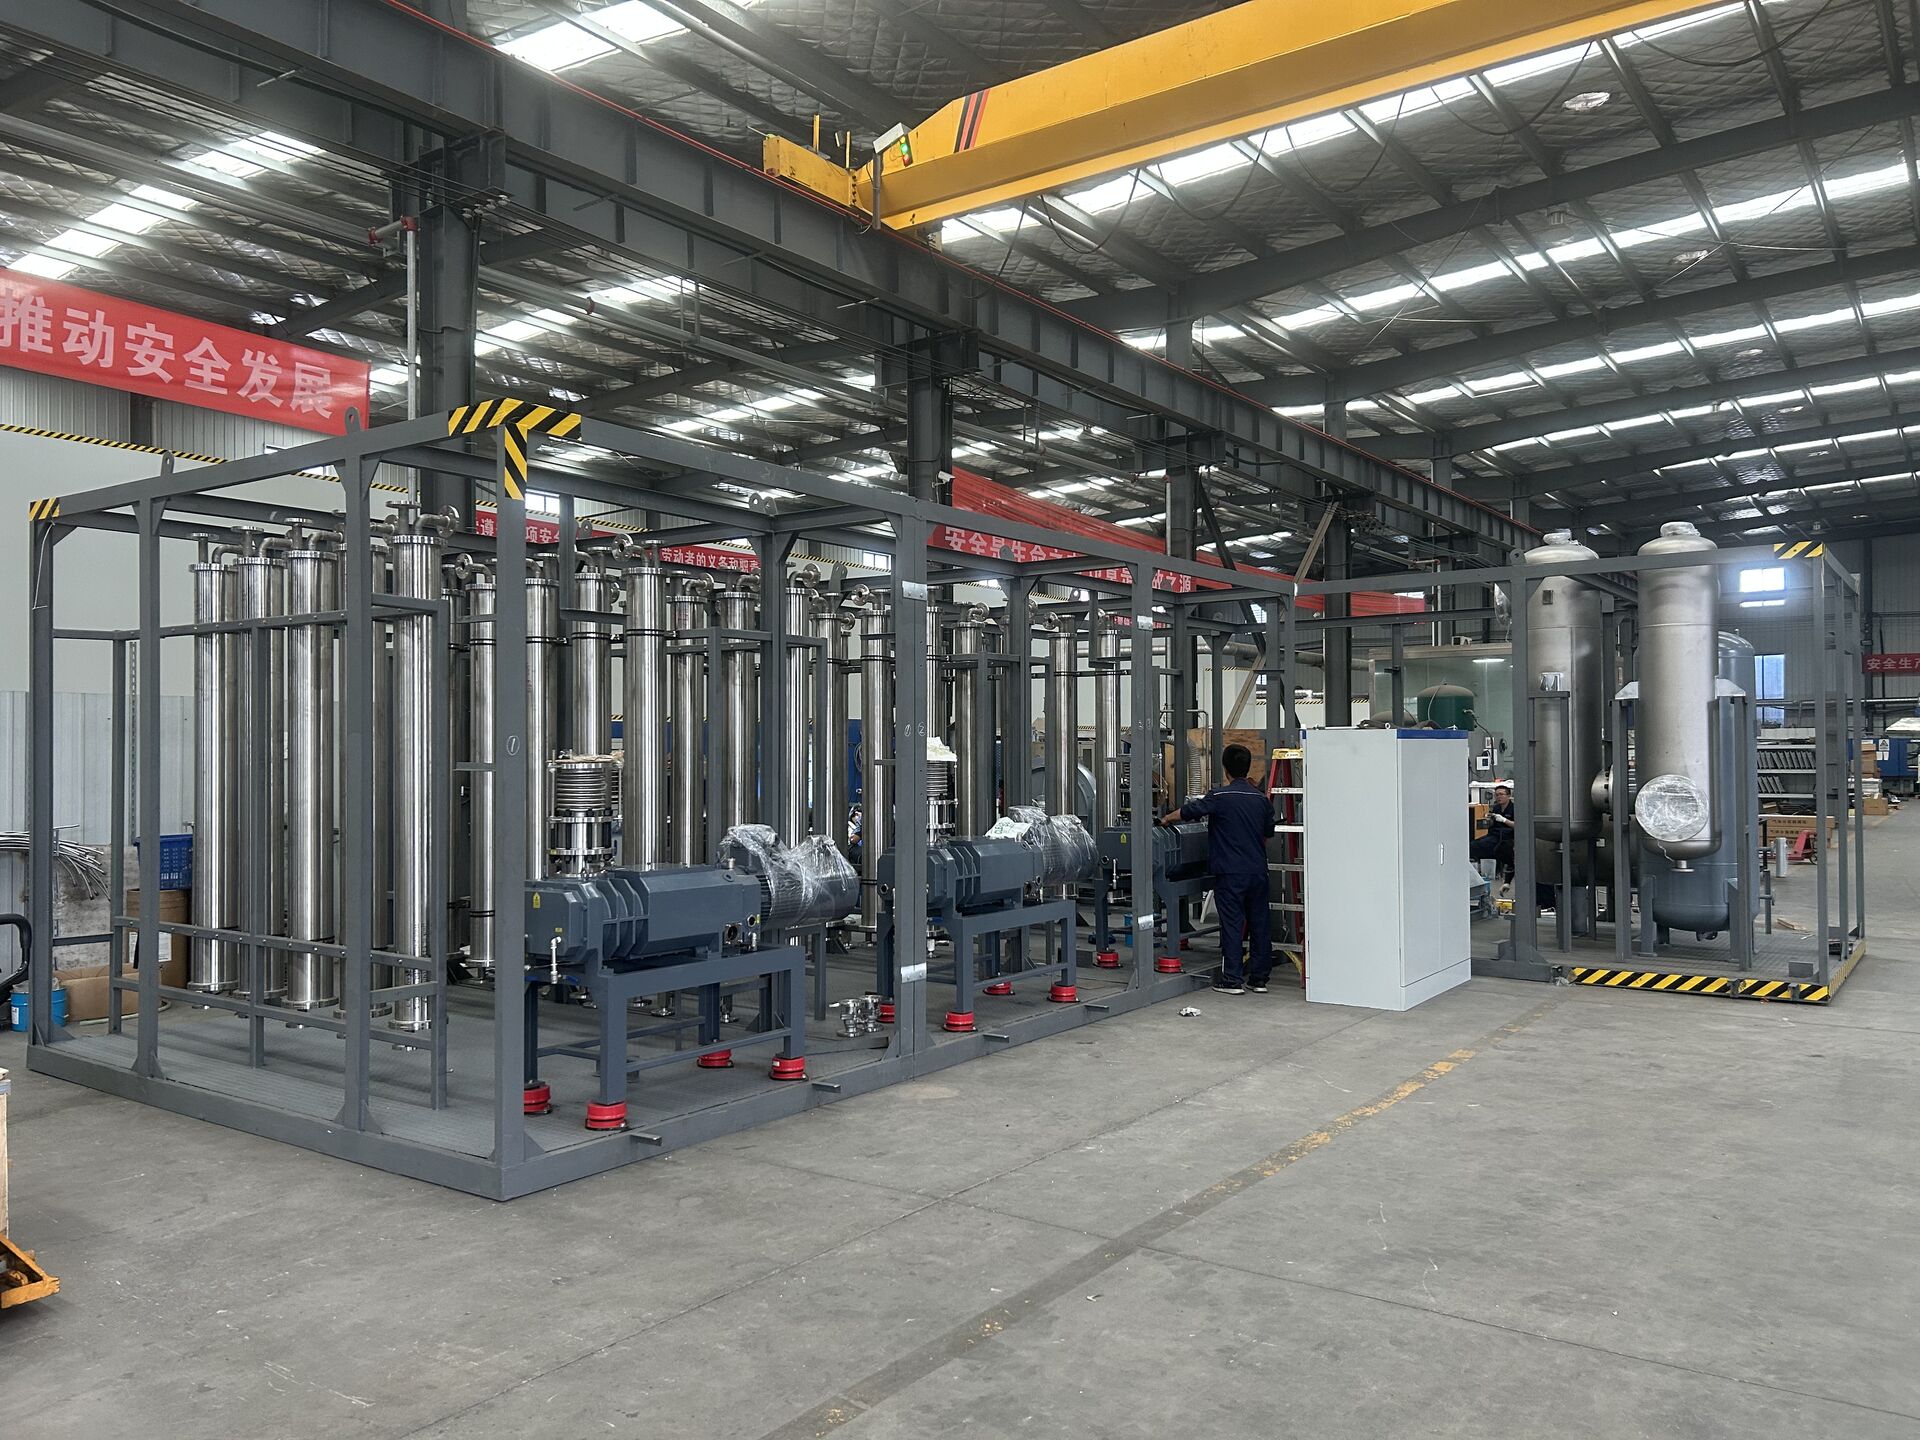
During the operation of the solvent recovery device, high boiling point residual liquid will gradually accumulate in the distillation kettle and evaporator: the solvent is evaporated out, impurities, oligomers and high boiling point components remain in the kettle, and the concentration is higher and higher, which affects heat transfer and product quality and must be discharged regularly. Kettle residue treatment seems to be just slag discharge. Poor arrangement will become a short board for stable operation of the device: the yield will be damaged if the discharge is early, the heat transfer will deteriorate if the discharge is late, and scaling will intensify.
Kettle residue management is a link that is rarely written on the table in solvent recovery operation: the manual talks about the process principle, and seldom talks about when, how much and how to discharge residual liquid. The long-term operation of the device will be much smoother if the residual management of the kettle is supplemented in the operation ledger.
The location of the residual liquid discharge port is also exquisite: it is close to the operation channel and far away from the electrical equipment. The placement and transfer route of the receiving container are determined in the layout stage, and detours are less during operation, and the discharge operation is safer.
There are three indicators to judge the timing of residue removal: the corresponding relationship between kettle temperature and kettle pressure drifts, and the kettle temperature rises under the same pressure, indicating that the concentration of residue rises; The heat transfer temperature difference increases, and the same evaporation amount requires a larger temperature difference. High boiling impurities rise in the quality test of recovered liquid. If any of the three indicators appears, arrange sampling analysis and determine the residual amount according to the analysis results.
Fixed-cycle residual is a common simplification: a cycle based on experience is set and scheduled as soon as it expires. The periodic method is simple to manage, but under the condition of large batch difference, the early and late rows are not accurate, and the occasions with analysis conditions are still arranged according to the index.
Discharge of residues is arranged in batch gaps or low load periods: the materials in the kettle are concentrated in place first, steam is cut off from the feed, and the residual liquid is discharged while it is hot-the temperature is low, the viscosity rises, and the discharge is not clean. The discharge line is kept short and straight, sloping towards the receiving vessel, with heat tracing as necessary. The residual liquid receiving container is sealed and marked. The solvent component in the residual liquid has recycling value and cannot be disposed of as waste at will.
The flushing link after residue removal is also important: the flushing liquid is collected and tested separately, the high solvent content is incorporated into the recovery process, and the solvent-free basically is treated as wastewater. The flushing is not complete, the residual liquid scales on the kettle wall, and the next start-up heat transfer starts from a low starting point.
The destination of the kettle residue is determined by the composition: the distillation system with high solvent content is collected again; If the solvent content is low but the calorific value is acceptable, it shall be connected with the fuel system. If it cannot be used, it shall be entrusted for disposal according to the requirements of hazardous waste. The destination is clear before discharge, and the documents in the receiving link correspond to the ledger.
| Residual liquid condition | Basis for judgment | Processing destination |
|---|---|---|
| High solvent content | distillation recovery economy | Secondary recovery of back distillation system |
| medium-low content | Calorific value available | Interface with fuel system |
| Basically no solvent | Analysis and confirmation | Treat as waste water |
| Containing special impurities | Identification of hazardous waste | Disposal entrusted to qualified units |
| scaling residual liquid | Heat transfer temperature difference increases | Flushing combined with mechanical cleaning |
| Flushing fluid | Detecting components | Incorporation of recycled or wastewater by content |
The analysis has the final say: the yield of secondary distillation of residual liquid with high solvent content is considerable, and most of them are cost-effective after accounting. If the content drops below a few percent, the energy consumption and duration of re-collection are not cost-effective and will be turned to fuel or disposal.
Abnormal, usually indicating the increase of incoming impurities or the failure of the front-end impurity removal link. Check the feed filtration and pretreatment links, check the detection method at the same time, and find the reason to readjust the cycle.
Depending on the composition and calorific value, direct combustion of residual liquid containing halogen and high nitrogen and sulfur has emission risk. First, do composition analysis, confirm the receiving standard with the fuel receiver, and then determine the destination.
This article by LuoyangWohong PetrochemicalEquipment Co., Ltd. arranges that the company provides design, manufacturing and operation and maintenance services for condensation recovery, membrane separation recovery and complete solvent recovery devices for chemical and pharmaceutical enterprises. If you need process evaluation or scheme configuration, please contact and exchange.
Mr. Li 13526990215
Hotline