
In the chemical industry, the management of VOCs (volatile organic compounds) in the storage tank area has always been a headache. These VOCs will not only cause environmental pollution, but also cause odor complaints, bringing a lot of trouble to the enterprise. So, how to effectively solve the chemical storage tank area VOCs governance problems, eliminate odor? Membrane condensation recovery technology may be a good solution.
Many enterprises in dealing with VOCs, there are many drawbacks in the traditional way. For exampleactivated charcoalAdsorption, a month to change carbon, carbon high cost, cumbersome procedures, and only the organic matter in the exhaust gas transferred to the carbon, the problem is not really solved;RTO(Regenerative Thermal Incinerator) Although the treatment effect of waste gas is good, the consumption of gas is high. When treating low-concentration waste gas, the burned gas is more valuable than the recovered solvent. If the operating load is reduced, the emission does not meet the standard. At the same time, it is a pity that the solvent in the waste gas is burned.
The membrane condensation recovery technology can effectively solve these problems. With LuoyangWohong PetrochemicalFor example, the membrane condensation recovery unit of Equipment Co., Ltd. uses three-stage condensation.gas separation membraneCombination process, suitable for chemical, pharmaceutical, gas station and other industries in the high concentration of organicwaste gas treatment. Its operating cost is low, the equipment only consumes electricity, the refrigeration compressor and vacuum pump are controlled by frequency conversion, which can automatically adjust the power according to the exhaust gas load and effectively control the power consumption.
At the same time, the technology is able to recover the solvent to create revenue. It condenses and liquefies the organic solvent in the exhaust gas for recovery, and the recovery purity can reach a higher level. The recovered solvent can be directly reused for production or external sales, and environmental protection expenditures can be converted into economic benefits. Moreover, the service life of the core consumable membrane component is longer. Daily maintenance is mainly to check the pressure and recovery liquid level of the refrigeration system every week, clean the heat exchanger fins every month, replace the freezing oil and dry filter every year, and there is no trouble of frequent replacement of consumables.
In addition, the equipment adopts a skid-mounted integrated design. All components are integrated on a stainless steel base. Assembly and testing are completed before leaving the factory. The site can be used only by connecting the power source and air duct. The installation period is short, the floor area is small, and explosion-proof configuration is optional. It is suitable for explosion-proof places such as chemical industry and pharmacy. The equipment has a wide range of applications, and has a good recovery effect on common organic solvents such as hydrocarbons, esters, ketones, alcohols, halogenated hydrocarbons, etc., and can be customized according to customer working conditions.
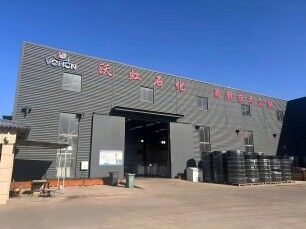
Relying on the R & D platform of Henan Oil and Gas Recovery Engineering Technology Research Center, Luoyang Wo Hong Petrochemical Equipment Co., Ltd. has set up a professional scientific research, manufacturing and marketing team, and designed a variety of technical solutions and equipment for VOCs waste gas recovery and treatment. The company focuses on close cooperation with customers, in-depth understanding of customer needs, to provide complete support from the early to the late. In the early stage, free working condition investigation and exhaust gas composition analysis will be provided, and targeted technical schemes and payback period calculation will be issued according to the three core parameters of concentration, air volume and composition. In the medium term, equipment manufacturing, factory testing, transportation, installation guidance, debugging and operator training will be provided. In the later period, one-year warranty, spare parts supply, remote technical support and regular inspection services will be provided. Customers can also sign long-term maintenance contracts as required.
In short, the membrane condensation recovery technology provides an efficient, economical and environmentally friendly solution for the treatment of VOCs in the chemical storage tank area, which can effectively solve the problem of odor complaints and help enterprises achieve green and sustainable development. Luoyang Wo Hong Petrochemical Equipment Co., Ltd. continues to innovate in this field to provide customers with high-quality products and services.
Mr. Li 13526990215

Hotline





